Leave Your Message
Precision-engineered packaging for the frozen food sector — combining multi-layer barrier technology, airtight sealing, and cold-resistant materials to protect your products at every stage of the cold chain.
The global frozen food packaging market is undergoing rapid transformation, driven by surging consumer demand, cold-chain infrastructure expansion, and tightening regulatory requirements worldwide.
Understanding the current state of the frozen food packaging industry helps brands, retailers, and manufacturers make smarter decisions about material selection, design, and supply chain strategy.
Frozen food packaging is far more than a container — it is the primary defense against freezer burn, moisture migration, microbial contamination, and mechanical damage throughout a product's entire cold-chain journey. As global frozen food consumption grows across retail, foodservice, and e-commerce channels, the packaging systems protecting these products must evolve in parallel. From advanced barrier laminates to intelligent smart-seal technologies, frozen food packaging bags sit at the intersection of food science, materials engineering, and brand communication.
Leading frozen food brands are increasingly partnering directly with specialized packaging manufacturers to reduce per-unit costs while improving customization capabilities. Large-scale rotogravure printers like Tianchen deliver consistent, high-volume output with tight color tolerances — essential for global brand consistency across markets.
China-based packaging factories have become indispensable in the global frozen food supply chain, offering cost efficiency, advanced manufacturing technology, and rapid prototyping. Guangdong province, in particular, serves as a world-class hub for flexible packaging export — connecting Asian manufacturers with buyers across Europe, North America, and Southeast Asia.
Food-contact regulations are tightening across the EU, US, and Asia-Pacific regions. Packaging materials used in frozen food applications must comply with FDA 21 CFR, EU Regulation 10/2011, GB standards in China, and other regional food safety frameworks — requiring certified suppliers with documented testing protocols and material traceability.
The next generation of frozen food packaging bags is being shaped by sustainability mandates, consumer behavior shifts, and breakthroughs in materials science and digital manufacturing.
Single-material mono-laminates and PCR (post-consumer recycled) content films are replacing traditional multi-layer non-recyclable structures. Packaging engineers are developing PE-based barrier solutions that maintain oxygen and moisture transmission performance at sub-zero temperatures while meeting circular economy standards set by brands like Nestlé, Unilever, and major retailers.
QR codes, NFC tags, and time-temperature indicators (TTIs) embedded in frozen food packaging bags are enabling real-time cold-chain monitoring, product authentication, and consumer engagement. These smart features are particularly valuable in premium frozen seafood, ready-meal, and pharmaceutical-adjacent categories where temperature deviation must be tracked and documented.
Advanced EVOH (ethylene vinyl alcohol), PVDC, and metallized PET/OPP structures are achieving oxygen transmission rates below 1 cc/m²/day — critical for frozen meat, seafood, and ready-to-cook products. These materials maintain their barrier integrity across the freeze-thaw cycles that stress conventional packaging structures, significantly extending product shelf life.
The explosive growth of online grocery and direct-to-consumer frozen food delivery has created demand for packaging that withstands not just retail freezer conditions, but also the mechanical stresses of automated warehouse sorting, last-mile delivery, and consumer home freezer storage. Reinforced seals, puncture-resistant substrates, and insulated pouch formats are gaining rapid market traction in this segment.
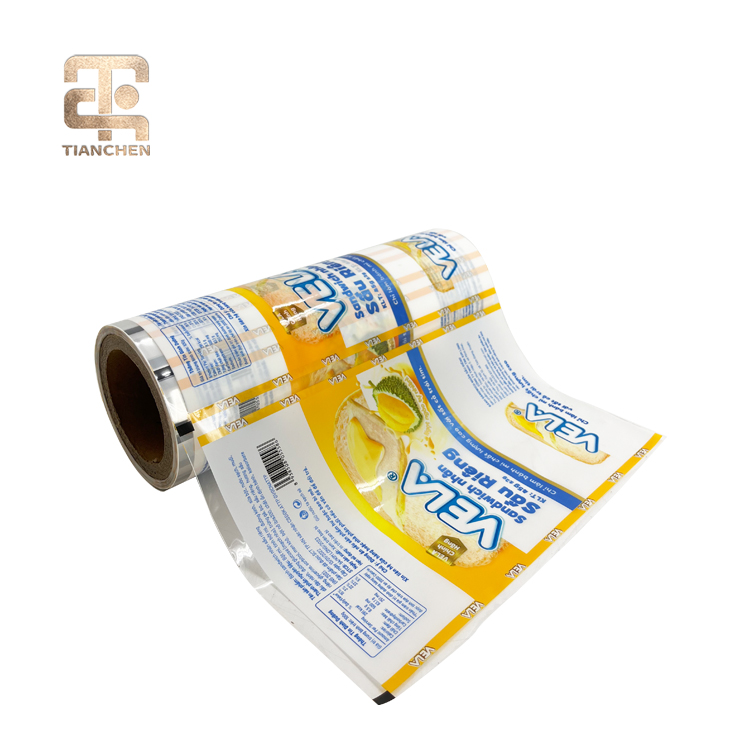
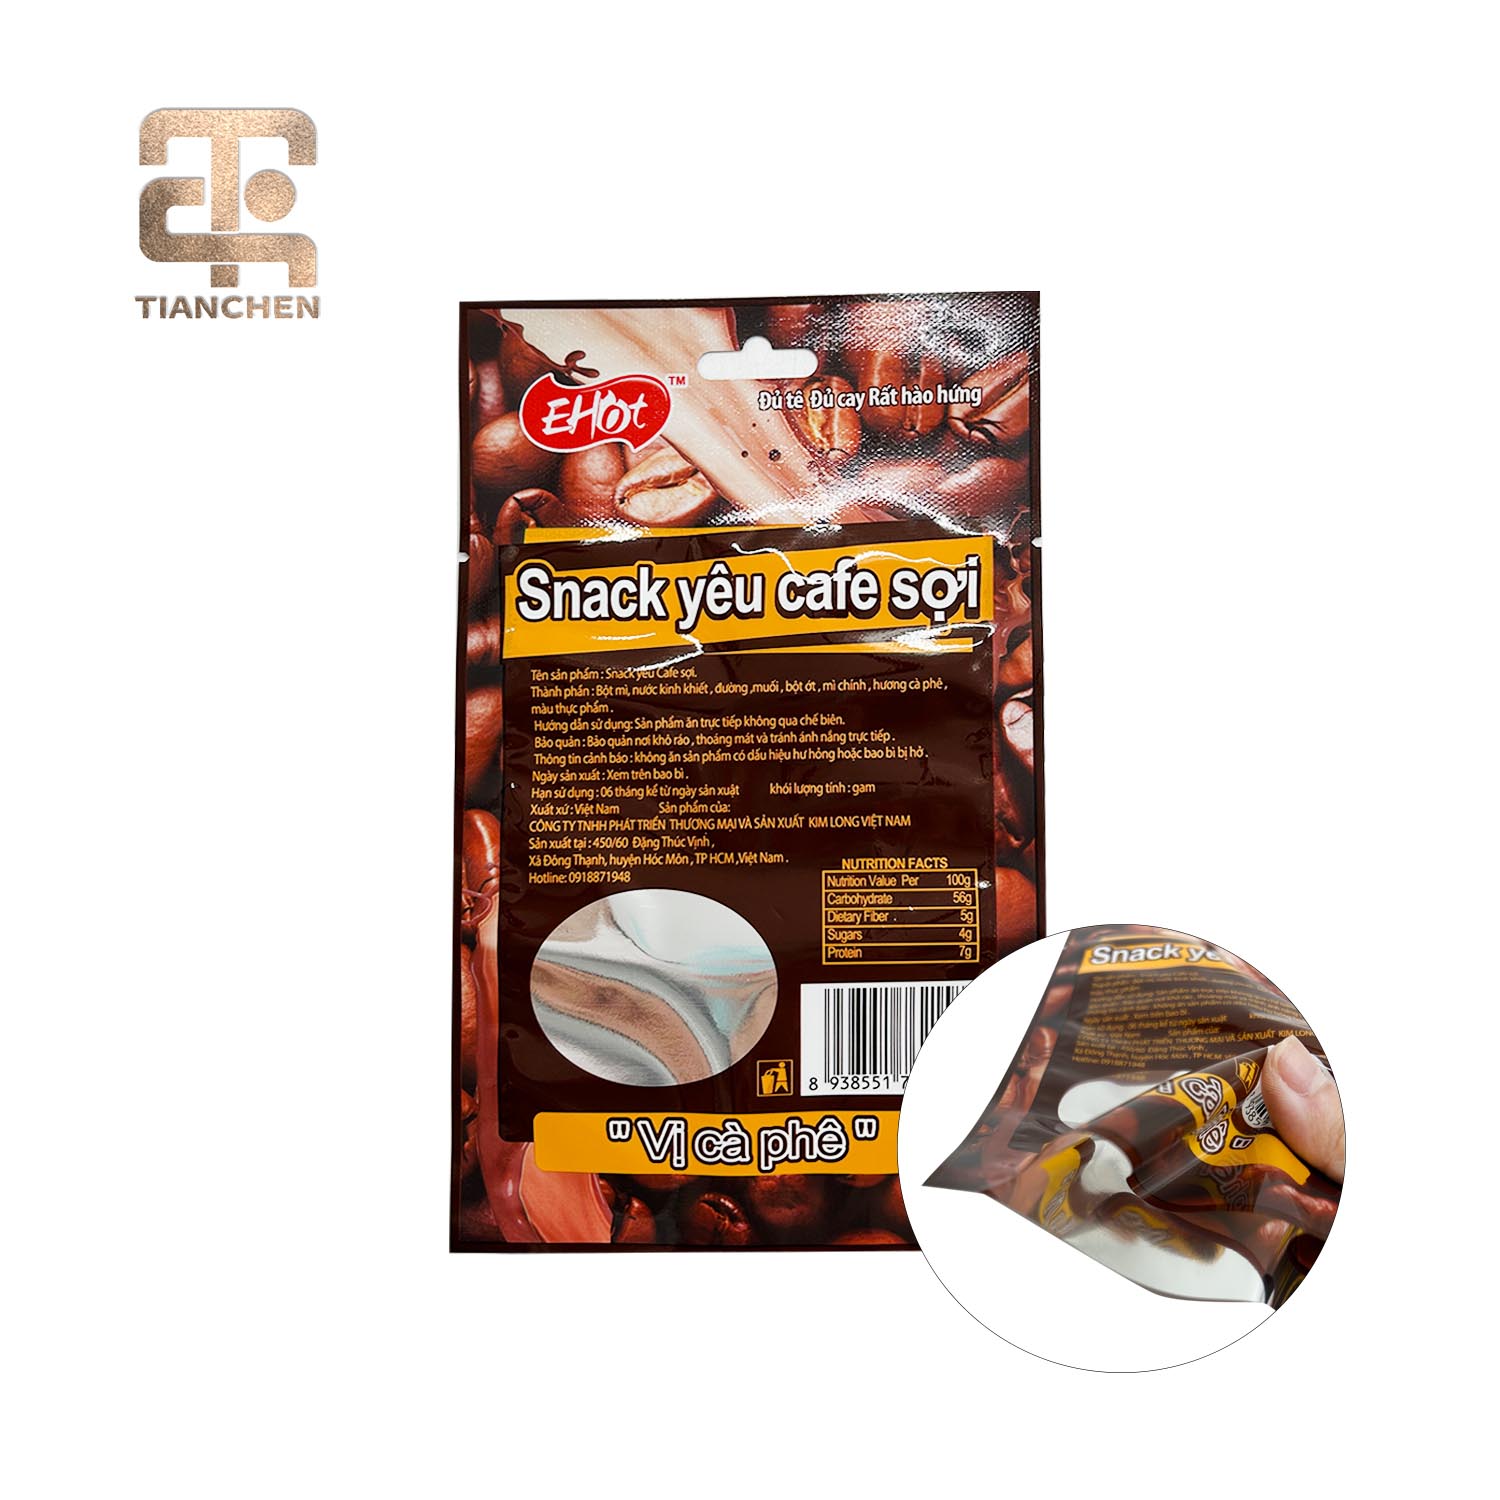
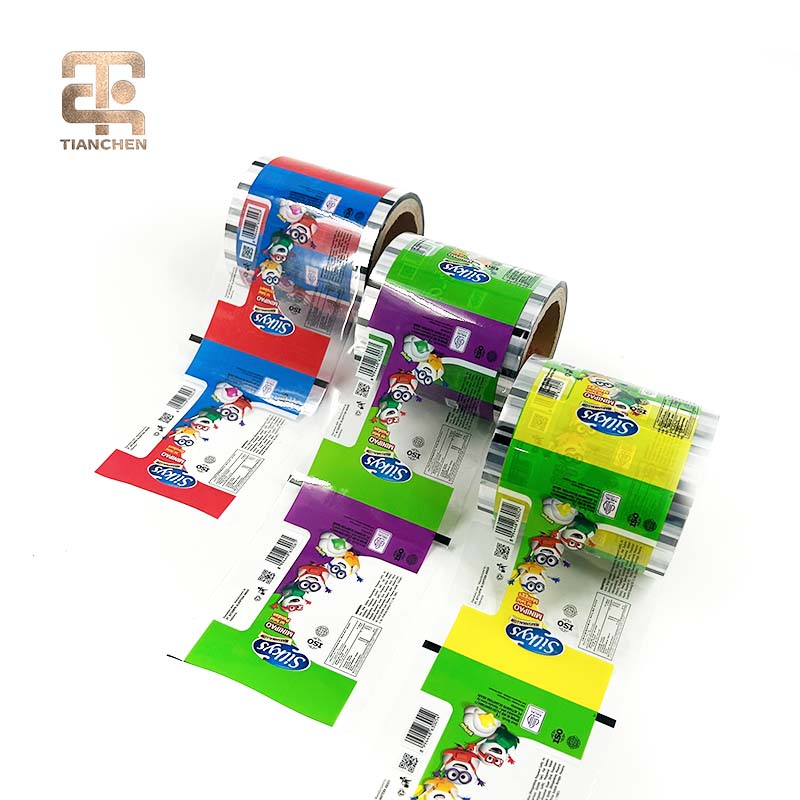
Rotogravure printing delivers photographic-quality graphics on frozen food packaging bags — enabling brands to communicate product quality, origin stories, nutritional claims, and sustainability credentials with vivid visual impact. Matte finishes, spot gloss effects, and metallic inks are increasingly used to differentiate premium frozen products at the retail shelf in competitive categories.
Certain frozen food products require packaging that can withstand not only deep freeze storage but also high-temperature retort sterilization during production. Advanced retort pouches — featuring nylon/PP or PET/Al/PP laminates — must maintain structural integrity and seal strength at temperatures up to 135°C, then perform reliably at -40°C in frozen distribution chains.
Different frozen food categories demand distinctly different packaging specifications. Here we explore the critical performance requirements and packaging solutions across the most important application segments.
Meat and seafood are among the most demanding frozen food packaging applications, requiring extremely low oxygen transmission, high puncture resistance to prevent bone or shell damage, and tight heat seals to prevent juice leakage during thawing.
The frozen ready meal segment demands packaging that can transition from freezer to microwave or oven without compromise — balancing barrier performance with microwave-safe, heat-resistant materials that maintain structural integrity during reheating.
Artisan frozen breads, croissants, pastries, and sandwiches require packaging that preserves freshness and texture through the freeze cycle while offering attractive retail presentation that communicates product quality to the consumer.
IQF (individually quick frozen) vegetables and fruits are typically packed in high-clarity or printed poly bags and stand-up pouches designed for both retail and foodservice channels, where volume efficiency and visual appeal are key commercial drivers.
Ice cream and frozen desserts require packaging solutions that resist the rapid temperature fluctuations of retail freezer cycling, maintain vibrant print quality under cold conditions, and present brand identity powerfully in highly competitive category shelving environments.
Catering companies, hotel chains, and food processors rely on heavy-duty frozen food packaging solutions designed for large-weight products, automated packing lines, and the rigors of bulk cold-chain logistics including palletized freezer storage and international shipping.
Your trusted flexible packaging partner for frozen food and beyond — combining 20+ years of deep industry expertise with global manufacturing standards.
We are a professional printing team boasting more than 20 years of profound experience in the flexible packaging industry. Rooted in Guangdong, a hub of manufacturing and international trade in China, Tianchen Printing has grown into a reliable partner for global clients by focusing on rotogravure printing, laminating, and converting services for flexible packaging solutions.
Our business covers a diverse range of industries worldwide, including food and beverage, pharmaceuticals, daily chemicals, electronics, and agriculture. We tailor packaging solutions to meet the unique needs of each sector, from moisture-proof packaging for snacks to high-barrier films for pharmaceuticals, ensuring product safety, shelf appeal, and transportation stability.
Over the years, we have established long-term cooperative relationships with clients from Europe, North America, Southeast Asia, and other regions, winning wide recognition for our consistent quality and professional service.

Innovation · Internationalization · Integration · Intelligentization — Four foundational pillars guiding Tianchen's leadership in flexible packaging manufacturing.
Persistent investment in R&D, upgrading printing technologies, and developing eco-friendly, high-performance packaging materials to keep pace with industry trends.
Adhering to global standards in production and management, obtaining international certifications, and expanding our global service network worldwide.
One-stop service model integrating design, printing, laminating, converting, and quality inspection — streamlining the production process for efficient delivery.
Advanced intelligent production equipment and digital management systems enabling automated operations in color matching and quality control for superior consistency.

Guided by our core four "IN" concepts, we have forged a clear development path and maintained steady growth in the competitive global market. Innovation drives our persistent investment in R&D, upgrading printing technologies and processes, and developing eco-friendly, high-performance packaging materials to keep pace with industry trends and client demands.
Internationalization means we adhere to global standards in production and management, obtain international certifications, and expand our global service network to integrate into the international mainstream market.

Integration refers to our one-stop service model integrating design, printing, laminating, converting, and quality inspection. By optimizing the industrial chain layout, we streamline the production process, reduce costs for clients, and ensure efficient delivery.
Intelligentization — we have introduced advanced intelligent production equipment and digital management systems, realizing automated operations in key links such as color matching and quality control, which improves production efficiency and product consistency.
Partner with Tianchen — China's trusted flexible packaging manufacturer — for customized frozen food packaging bags that meet the highest international quality and food safety standards.
Request a Custom Quote Today →Explore our full portfolio of flexible packaging solutions designed for every frozen food application — from retail consumer packs to industrial bulk formats.