Leave Your Message
The beverage and juice industry has undergone a remarkable transformation over the past two decades, with laminated film technology emerging as a cornerstone of modern packaging solutions. As consumer preferences shift toward convenience, sustainability, and product freshness, beverage brands are increasingly relying on advanced laminated films to meet these evolving demands. These multi-layer structures combine different materials—typically polyethylene (PE), polyethylene terephthalate (PET), aluminum foil, and specialized barrier coatings—to create packaging that protects contents from oxygen, moisture, light, and contamination while maintaining visual appeal and structural integrity.
The global flexible packaging market for beverages is projected to reach $68.5 billion by 2028, with laminated films accounting for a significant portion of this growth. This expansion is driven by several factors: the rise of on-the-go consumption patterns, increasing demand for single-serve portions, growing awareness of food safety standards, and the beverage industry's push toward lightweight, recyclable packaging alternatives. Laminated films offer beverage brands a competitive advantage through superior barrier properties, extended shelf life, reduced transportation costs, and enhanced brand differentiation through high-quality printing capabilities.
According to recent market research, over 65% of juice and beverage manufacturers have transitioned to laminated film packaging in the past five years, citing improved product preservation, cost efficiency, and consumer appeal as primary motivators. The technology has proven particularly effective for cold-pressed juices, functional beverages, and premium drink categories where maintaining nutritional integrity and flavor profile is paramount.
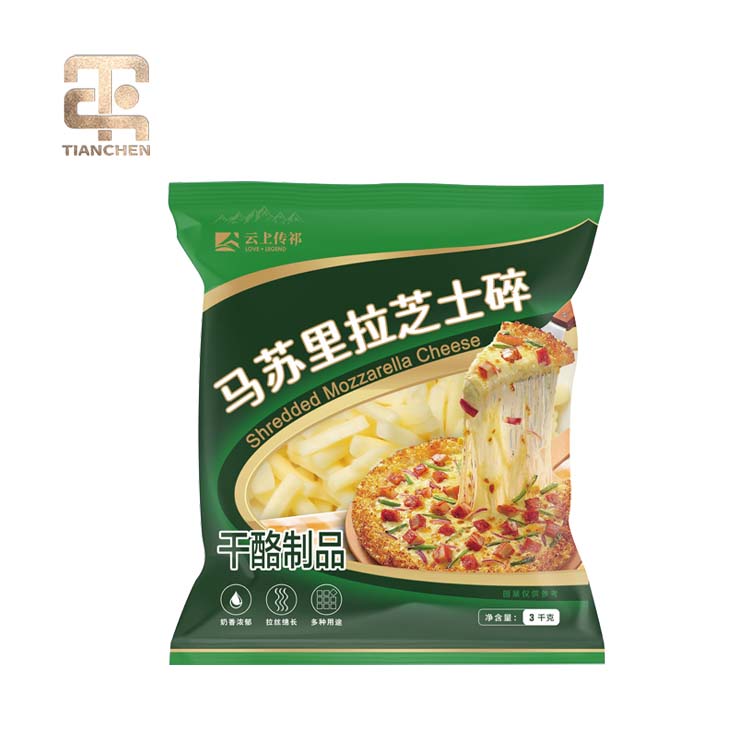
Laminated films provide excellent oxygen and light barriers for fresh and concentrated juices, preserving vitamins and natural flavors while offering convenient, portable packaging formats for children and adults.
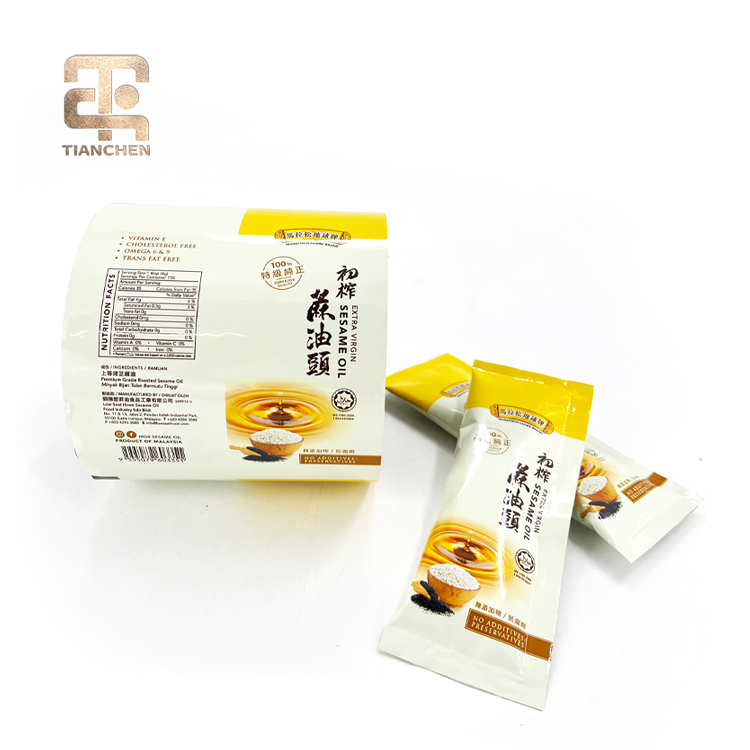
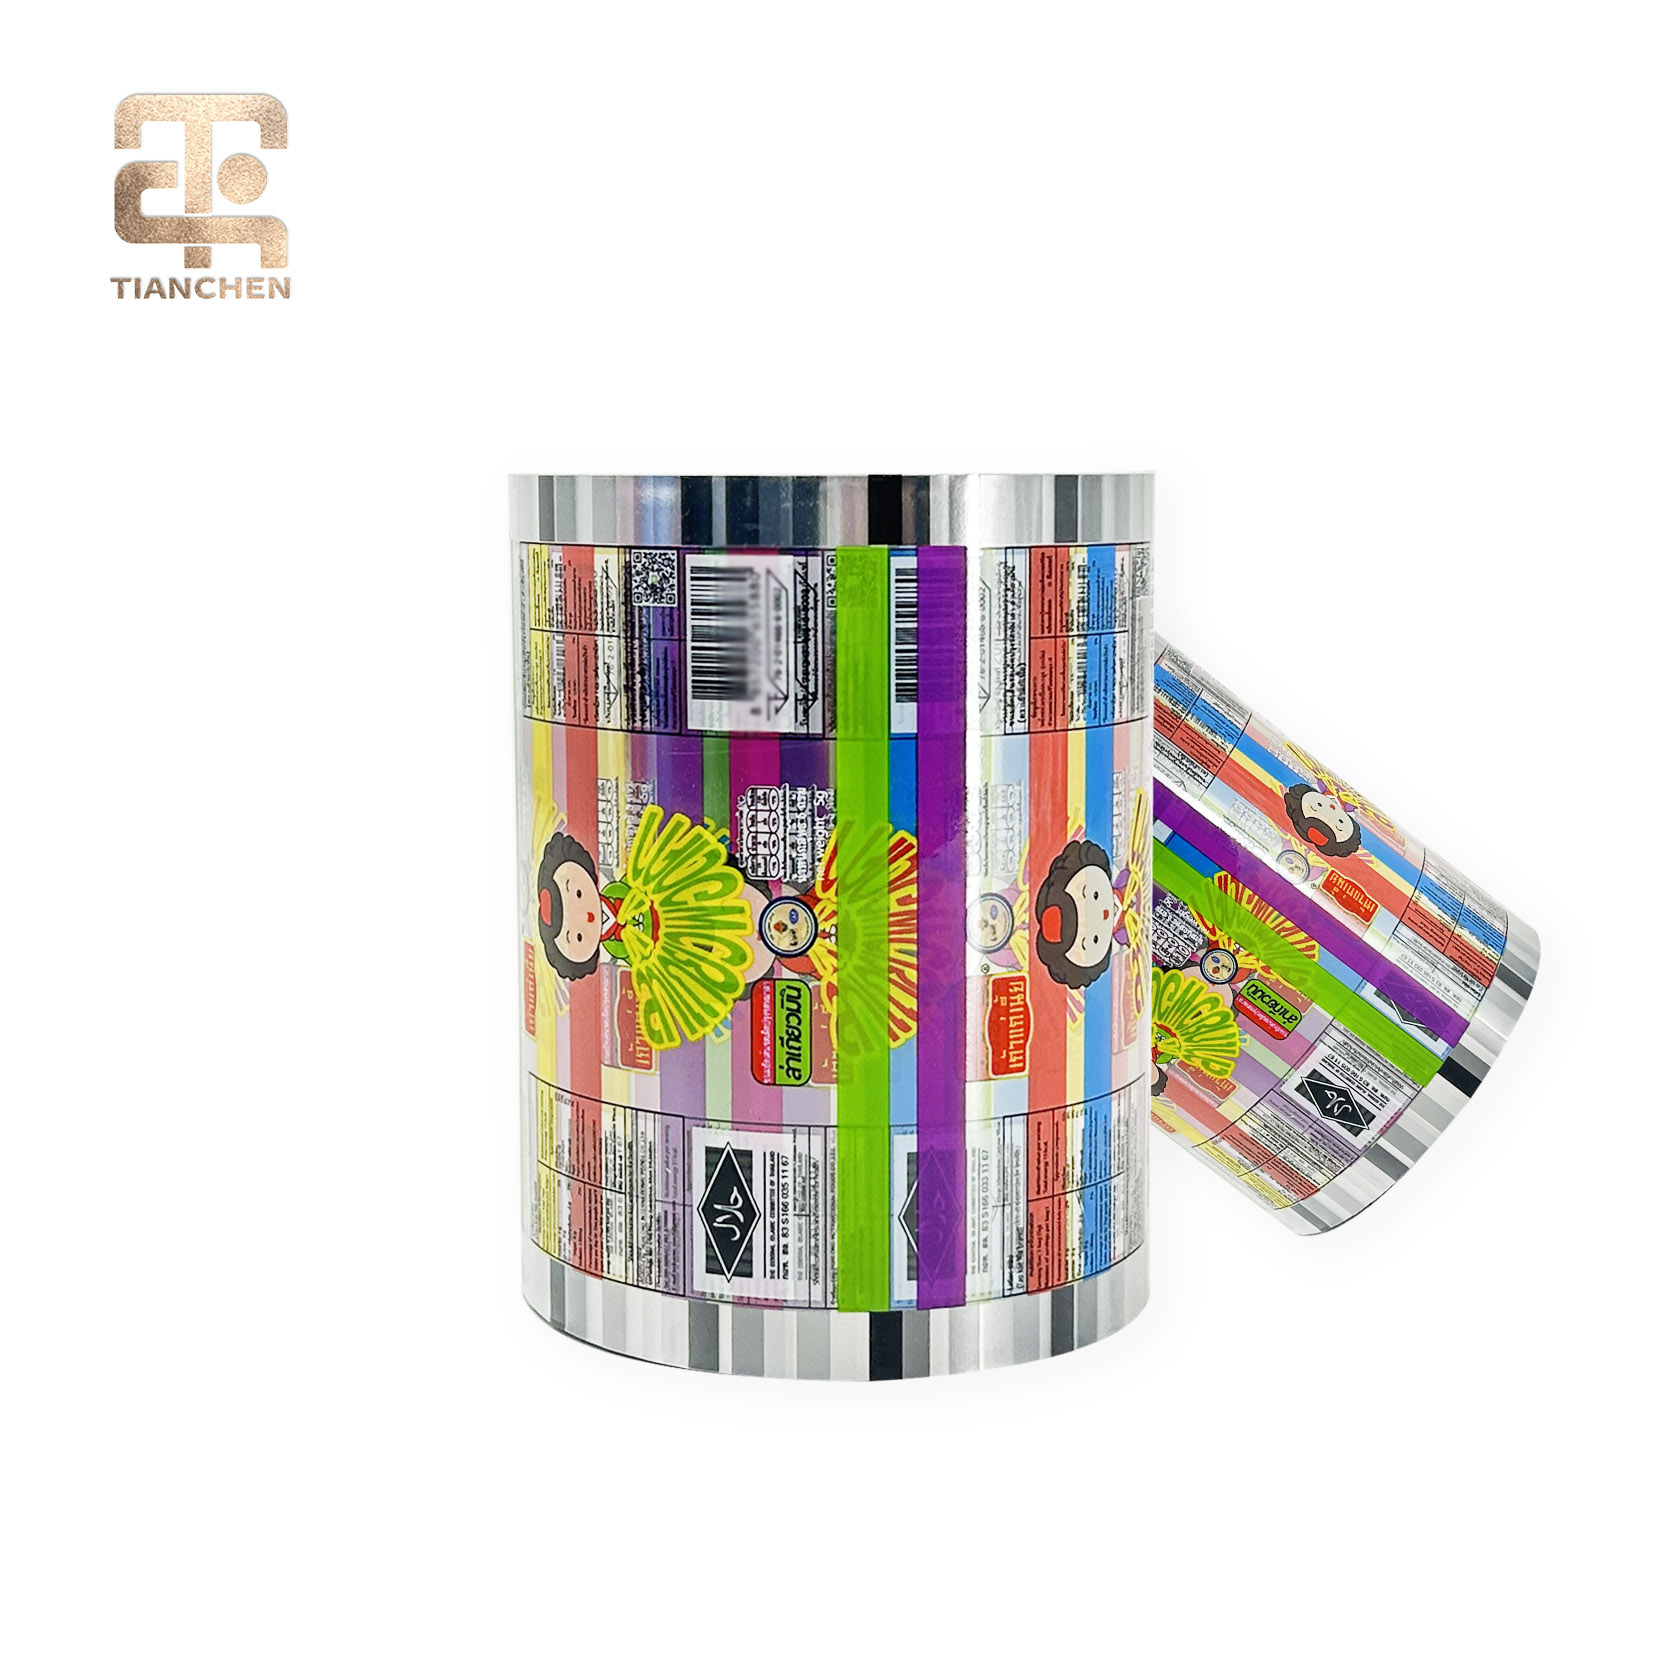
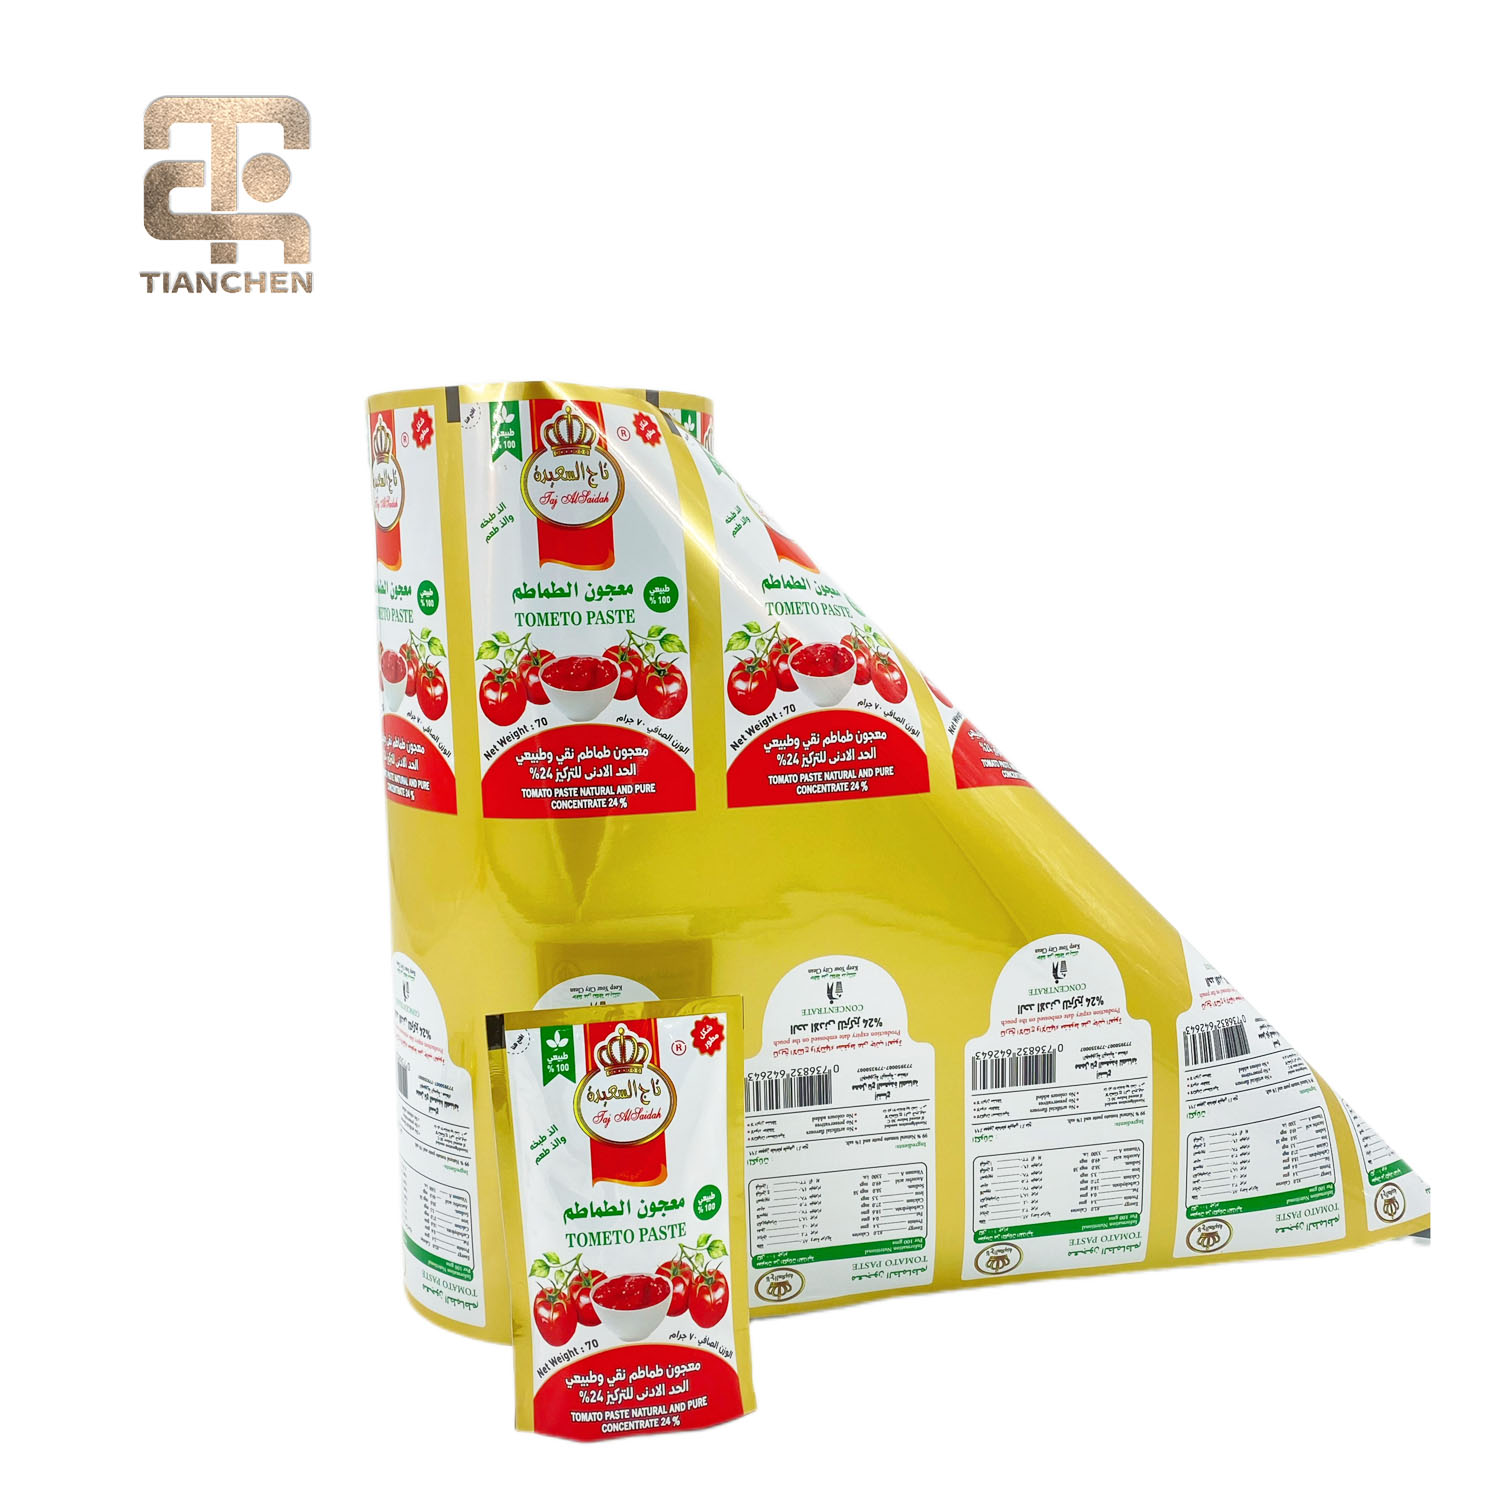
High-definition gravure printing on laminated films enables vibrant, eye-catching designs that enhance brand recognition on store shelves while maintaining durability through distribution and refrigeration.
Specialized barrier films protect sensitive ingredients in energy drinks, protein shakes, and wellness beverages from oxidation and degradation, ensuring product efficacy throughout the supply chain.
Clean-label laminated films without harmful additives meet the stringent requirements of organic certification while providing the necessary protection for preservative-free formulations.
Temperature-resistant laminated structures maintain seal integrity and barrier properties throughout refrigerated storage and transportation, preventing condensation-related quality issues.
Next-generation mono-material and recyclable laminated films address environmental concerns while maintaining the performance characteristics required for beverage packaging applications.
The versatility of laminated film technology allows beverage brands to address diverse packaging challenges across product categories. For cold-pressed juices, which contain no preservatives and require strict oxygen barriers to prevent enzymatic browning and nutrient degradation, multi-layer laminated structures incorporating EVOH (ethylene vinyl alcohol) or metallized layers provide exceptional protection. These films can extend shelf life from days to weeks, enabling broader distribution networks and reducing food waste.
Sports and energy drinks benefit from laminated films that resist puncture and abrasion during active use scenarios while maintaining seal integrity under varying temperature conditions. The incorporation of easy-open features, resealable closures, and ergonomic spout designs enhances user experience without compromising package integrity. Premium beverage brands leverage the superior printing capabilities of laminated films to create sophisticated visual presentations that communicate brand values and product attributes, from metallic finishes to matte textures and holographic effects.
The beverage packaging landscape is experiencing rapid transformation driven by technological innovation, regulatory pressures, and shifting consumer expectations. Sustainability has emerged as the dominant trend, with major beverage corporations committing to ambitious recyclability and carbon reduction targets. This has accelerated development of mono-material laminated films that can be processed through existing recycling infrastructure, as well as bio-based alternatives derived from renewable resources like sugarcane and corn starch.
The adoption of digital printing technologies for laminated films is revolutionizing beverage packaging by enabling short-run production, personalized designs, and rapid market testing. Brands can now launch limited editions, regional variations, and promotional campaigns without the high setup costs associated with traditional gravure printing, fostering innovation and consumer engagement.
Integration of QR codes, NFC tags, and time-temperature indicators into laminated films creates interactive consumer experiences while providing supply chain visibility. These technologies enable authentication, traceability, and real-time quality monitoring, addressing concerns about counterfeiting and product integrity in premium beverage segments.
Advanced lamination techniques and thinner gauge materials reduce packaging weight by 20-30% without compromising performance, delivering significant cost savings in transportation and raw materials while reducing environmental footprint. This trend aligns with corporate sustainability goals and regulatory requirements for packaging reduction across major markets.
Emerging coating technologies including atomic layer deposition (ALD) and plasma-enhanced chemical vapor deposition (PECVD) are enabling ultra-thin barrier layers with unprecedented oxygen and moisture transmission rates. These innovations allow beverage brands to achieve extended shelf life targets with thinner, lighter, and more sustainable laminated film structures.
The Asia-Pacific region, particularly China, has established itself as the global epicenter of laminated film manufacturing for beverage packaging. With its advanced production infrastructure, skilled workforce, and competitive cost structure, Chinese manufacturers are supplying premium laminated films to beverage brands across Europe, North America, Southeast Asia, and emerging markets. The region's manufacturing ecosystem supports rapid prototyping, flexible order quantities, and customization capabilities that global beverage brands require to stay competitive in fast-moving markets.
Regulatory developments are also shaping the laminated film industry for beverages. Stricter food contact material regulations in the European Union, United States, and other major markets are driving manufacturers to reformulate inks, adhesives, and coating materials to comply with updated safety standards. This regulatory pressure, while challenging, is ultimately elevating quality standards across the industry and creating opportunities for manufacturers who invest in compliance and certification.
Understanding the technical composition of laminated films is essential for beverage brands seeking to optimize their packaging performance. The most common structures used in beverage and juice packaging include PET/AL/PE (polyester/aluminum/polyethylene) for maximum barrier protection, BOPP/PE (biaxially oriented polypropylene/polyethylene) for transparent applications requiring moisture resistance, and PET/VMPET/PE (polyester/metallized polyester/polyethylene) for cost-effective barrier solutions with attractive metallic aesthetics.
The selection of laminated film structure for beverage packaging requires careful consideration of multiple performance parameters. Oxygen Transmission Rate (OTR) determines how quickly oxygen permeates the packaging, directly impacting product oxidation and shelf life. For sensitive juice products, OTR values below 0.5 cc/m²/day are typically required. Water Vapor Transmission Rate (WVTR) affects moisture exchange, critical for maintaining product concentration and preventing label degradation in refrigerated environments.
Seal strength and hot-tack properties determine packaging integrity during high-speed filling operations, while puncture resistance and tensile strength ensure durability throughout distribution. Laminated films must also demonstrate compatibility with various sterilization methods including pasteurization, UV treatment, and high-pressure processing (HPP) increasingly adopted by premium juice brands.
The printing layer of laminated films for beverage packaging deserves particular attention. Rotogravure printing, the technology of choice for high-volume beverage packaging, delivers exceptional color consistency, fine detail reproduction, and metallic effects that create premium shelf presence. With up to 12 color stations and registration accuracy within ±0.1mm, modern gravure printing presses produce packaging that meets the exacting standards of global beverage brands. Water-based and UV-curable inks are increasingly replacing solvent-based systems, reducing VOC emissions and improving the sustainability profile of laminated beverage packaging.


We are a professional printing team boasting more than 20 years of profound experience in the flexible packaging industry. Rooted in Guangdong, a hub of manufacturing and international trade in China, Tianchen Printing has grown into a reliable partner for global clients by focusing on rotogravure printing, laminating, and converting services for flexible packaging solutions.
Our business covers a diverse range of industries worldwide, including food and beverage, pharmaceuticals, daily chemicals, electronics, and agriculture. We tailor packaging solutions to meet the unique needs of each sector, from moisture-proof packaging for snacks to high-barrier films for pharmaceuticals, ensuring product safety, shelf appeal, and transportation stability. Over the years, we have established long-term cooperative relationships with clients from Europe, North America, Southeast Asia, and other regions, winning wide recognition for our consistent quality and professional service.
Innovation, Internationalization, Integration, Intelligentization
Guided by our core four "IN" concepts, we have forged a clear development path and maintained steady growth in the competitive global market. We persist in investing in R&D, upgrading printing technologies and processes, and developing eco-friendly, high-performance packaging materials to keep pace with industry trends and client demands. For beverage brands specifically, this means continuously improving barrier performance, seal reliability, and print quality to meet the most demanding product protection requirements.
We adhere to global standards in production and management, obtain international certifications, and expand our global service network to integrate into the international mainstream market. Our laminated films for beverage and juice brands comply with FDA, EU food contact regulations, and other major international standards, giving global beverage companies the confidence to source from us for their most demanding markets.
Our one-stop service model integrating design, printing, laminating, converting, and quality inspection streamlines the production process for beverage brands. By optimizing the industrial chain layout, we reduce costs for clients and ensure efficient delivery. Beverage companies benefit from a single trusted partner who understands every aspect of their packaging requirements, from initial concept to finished roll stock ready for high-speed filling lines.
We have introduced advanced intelligent production equipment and digital management systems, realizing automated operations in key links such as color matching and quality control, which improves production efficiency and product consistency. For beverage brand customers, this translates to tighter color tolerances, more consistent seal quality, and reliable batch-to-batch performance that protects brand integrity across large production volumes.
The future of laminated film technology for beverage and juice brands is being shaped by three converging forces: sustainability imperatives, performance demands, and digitalization. As major beverage corporations commit to ambitious environmental targets—including 100% recyclable or reusable packaging by 2030—the flexible packaging industry is accelerating development of next-generation laminated structures that balance ecological responsibility with functional performance.
Bio-based and compostable laminated films are moving from laboratory development to commercial scale, with several beverage brands already piloting plant-based packaging for premium juice lines. These materials, derived from renewable resources like PLA (polylactic acid) and PHA (polyhydroxyalkanoates), offer comparable barrier properties to conventional petroleum-based films while significantly reducing carbon footprint. As production costs decrease with scale, bio-based laminated films are expected to capture a growing share of the beverage packaging market.
The integration of nanotechnology into laminated film structures represents another frontier of innovation. Nano-clay composites and graphene-based coatings are demonstrating exceptional barrier properties at minimal thickness, potentially enabling the development of high-performance beverage packaging with reduced material usage. These advanced materials also offer antimicrobial properties that could extend product shelf life without the need for chemical preservatives, aligning with clean-label trends in the premium juice segment.
Artificial intelligence and machine vision systems are transforming quality control in laminated film production, enabling 100% inspection of printed graphics, seal integrity, and material defects at production speeds exceeding 300 meters per minute. This technological advancement ensures that beverage brands receive packaging that consistently meets their quality specifications, reducing waste and protecting brand reputation in an increasingly competitive marketplace.