Leave Your Message
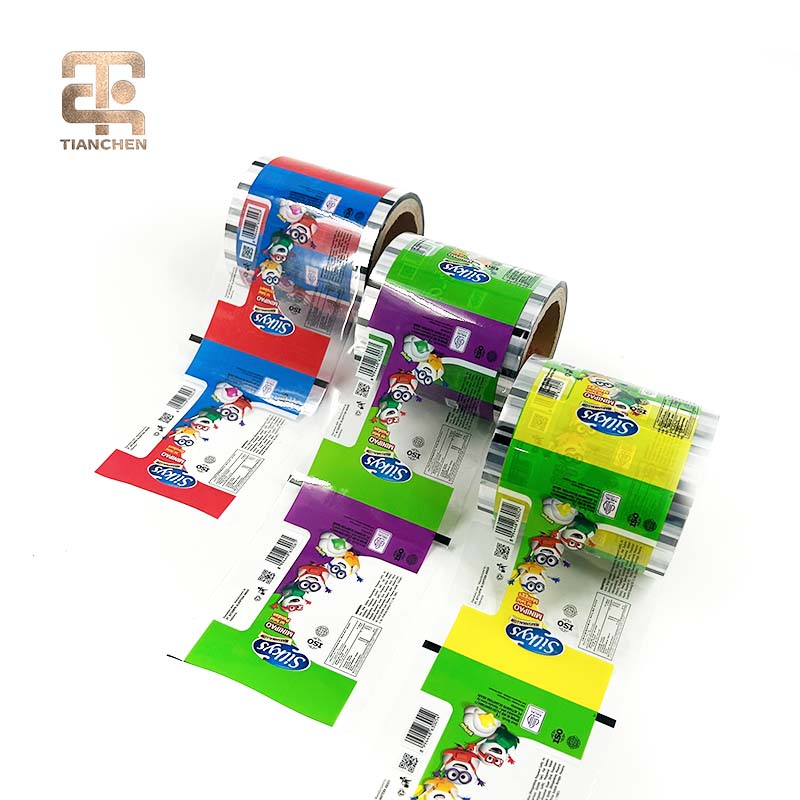
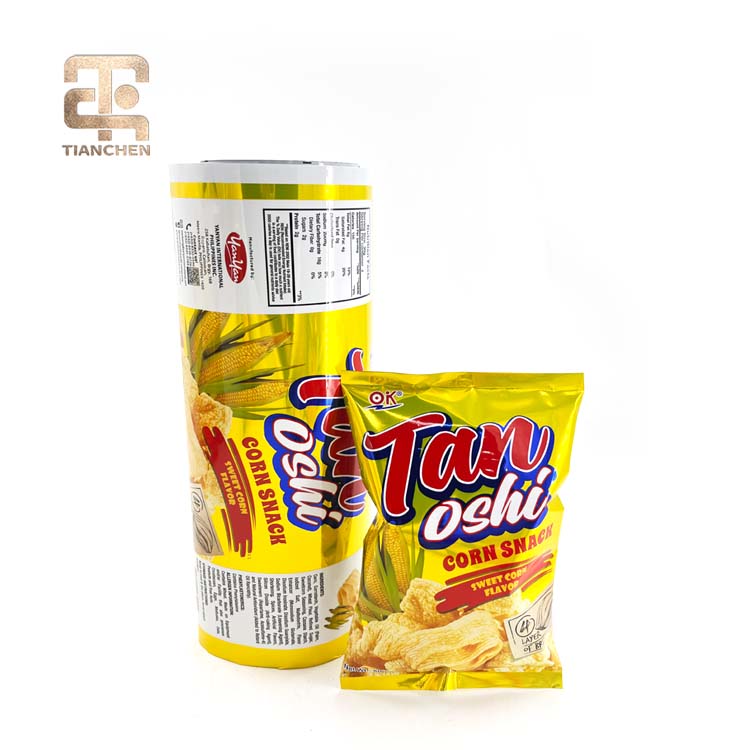
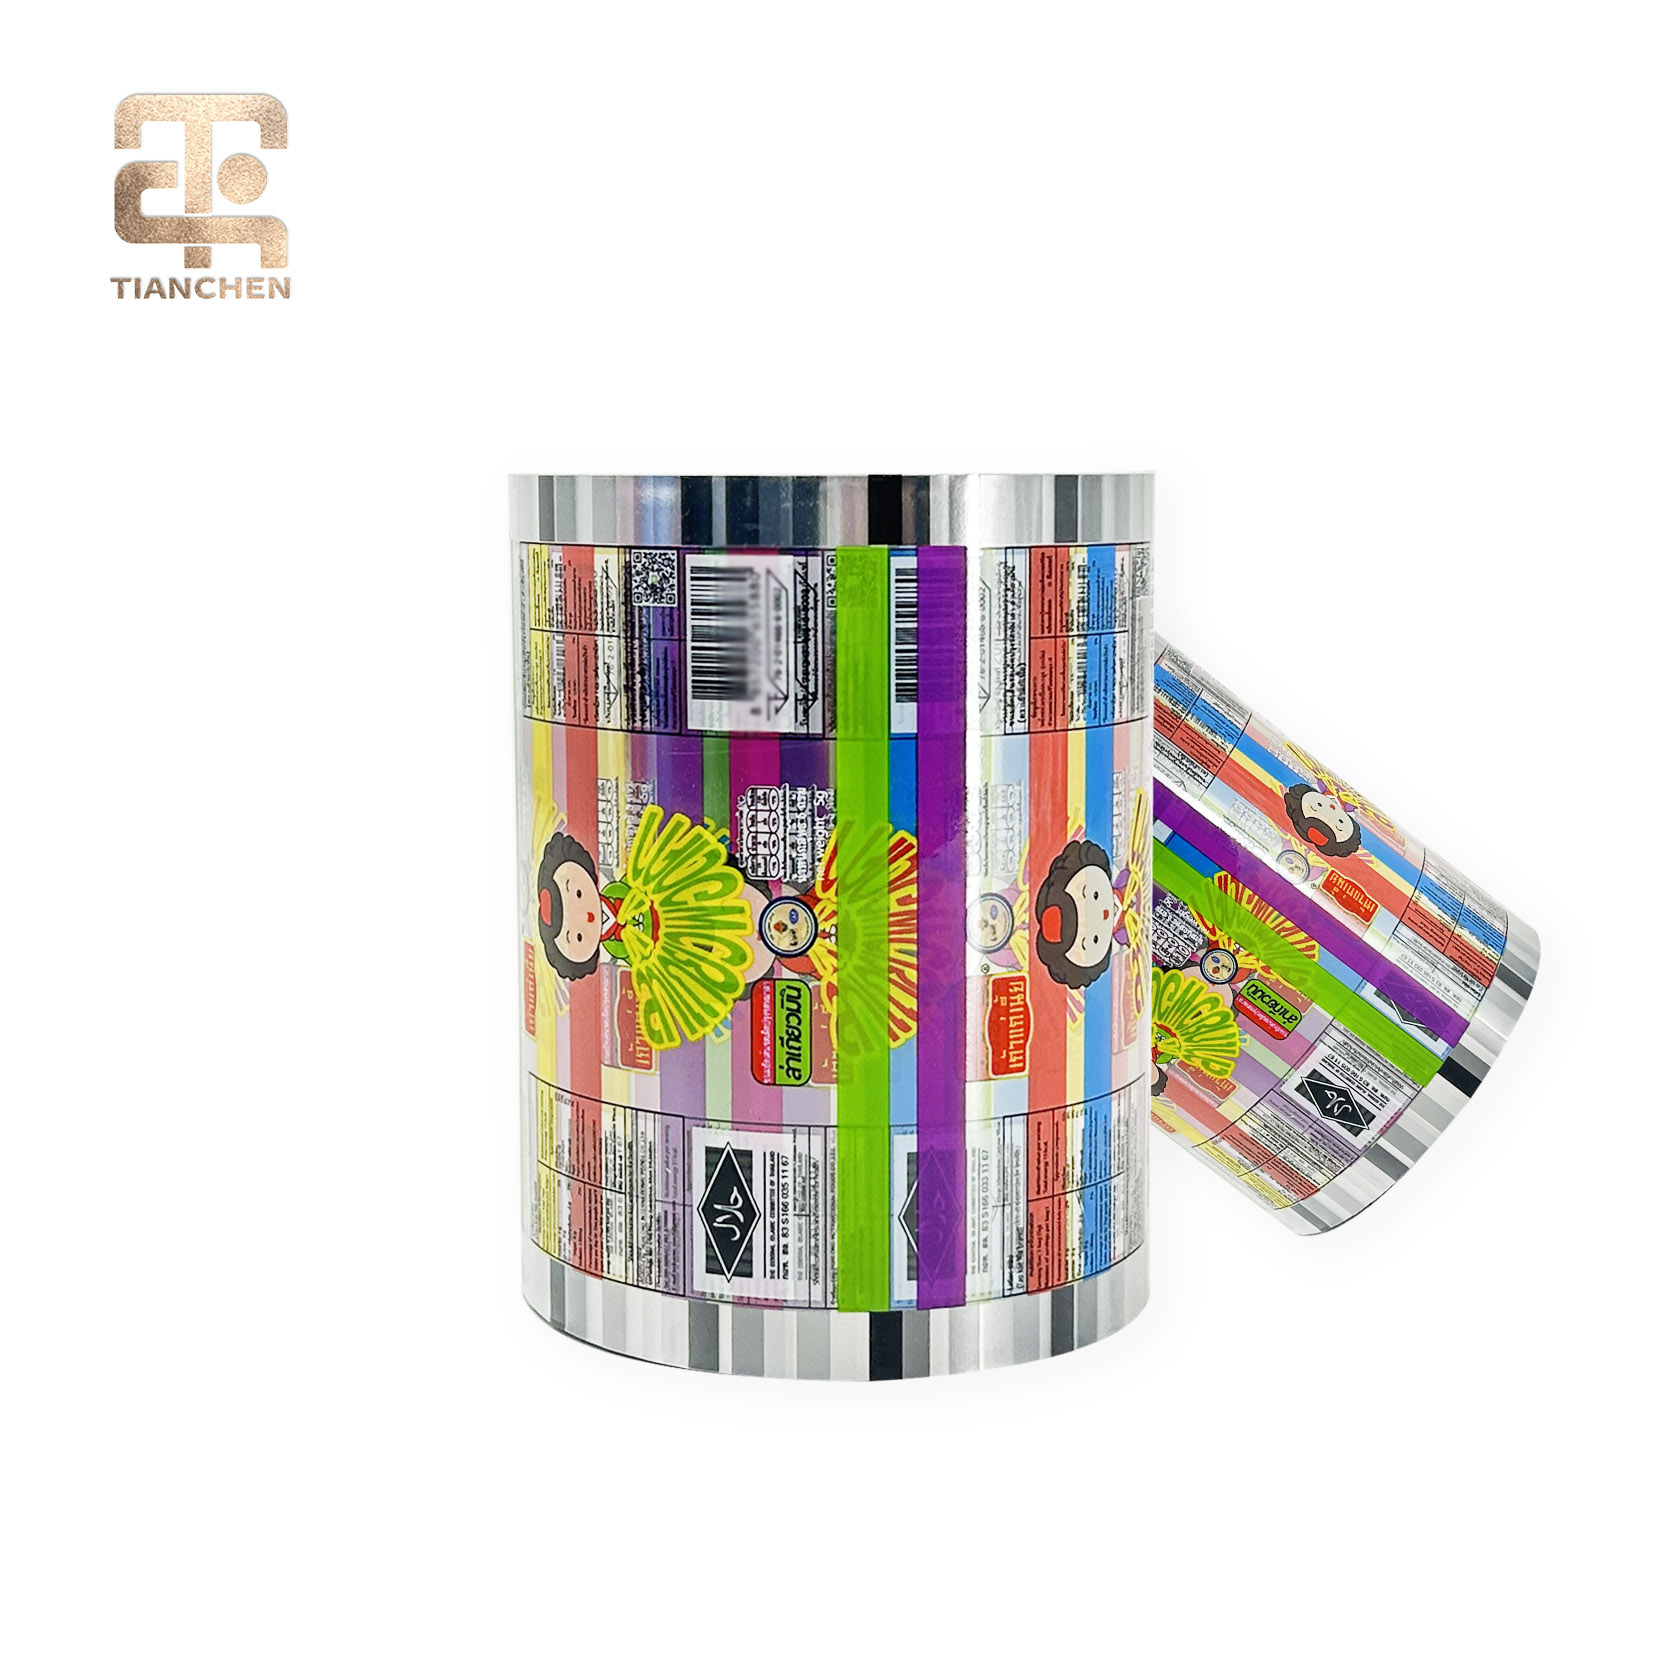
Precision-engineered laminated films designed specifically for snack food packaging — moisture-proof, high-barrier, and custom-printed for maximum shelf appeal.
Global demand for high-performance laminated film in snack food manufacturing is accelerating — driven by evolving consumer behavior, stricter food safety standards, and the rise of e-commerce retail.
The global flexible packaging market was valued at over USD 200 billion in 2024, with snack food packaging representing one of the fastest-growing segments. As consumers worldwide demand greater convenience, longer shelf life, and more visually compelling products, snack food manufacturers face mounting pressure to adopt advanced laminated film technologies that deliver on all fronts — barrier protection, printability, seal integrity, and sustainability.
Laminated film — a composite material formed by bonding two or more layers of polymer films, aluminum foil, or paper — has become the industry-standard packaging substrate for chips, crackers, nuts, dried fruits, confectionery, baked goods, and countless other snack categories. Its ability to combine the individual strengths of each layer (e.g., the oxygen barrier of aluminum foil, the moisture resistance of PE, and the structural rigidity of PET) makes it uniquely suited to the demanding requirements of snack food production lines.
Asia-Pacific — led by China — accounts for the largest share of global flexible packaging production, with Guangdong province alone hosting hundreds of world-class rotogravure printing and laminating facilities. Chinese manufacturers supply laminated film to snack brands across Europe, North America, Southeast Asia, the Middle East, and beyond, combining competitive pricing with increasingly sophisticated technical capabilities.
Modern snack production lines run at speeds exceeding 800 bags/min. Laminated films must deliver consistent thickness, tensile strength, and slip properties to ensure zero-downtime performance on VFFS and HFFS machines.
Regulatory pressure and consumer awareness are driving rapid adoption of recyclable mono-material laminates, compostable films, and reduced-thickness structures — without compromising barrier or seal performance.
With thousands of SKUs competing on shelf, snack brands increasingly rely on 10-color rotogravure printing, metallic effects, matte/gloss contrasts, and tactile finishes on laminated film to capture consumer attention.
High-barrier laminated structures combining BOPP, BOPA, aluminum foil, and PE layers achieve oxygen transmission rates below 1 cc/m²/day — critical for preserving the crunch, flavor, and nutritional value of snack products.
The explosive growth of online snack retail demands packaging with superior puncture resistance, resealability, and aesthetic appeal that survives the rigors of last-mile logistics while delighting the unboxing experience.
Next-generation laminated films are incorporating QR code integration, freshness indicators, and nano-barrier coatings — enabling snack brands to build digital engagement and real-time supply chain traceability.
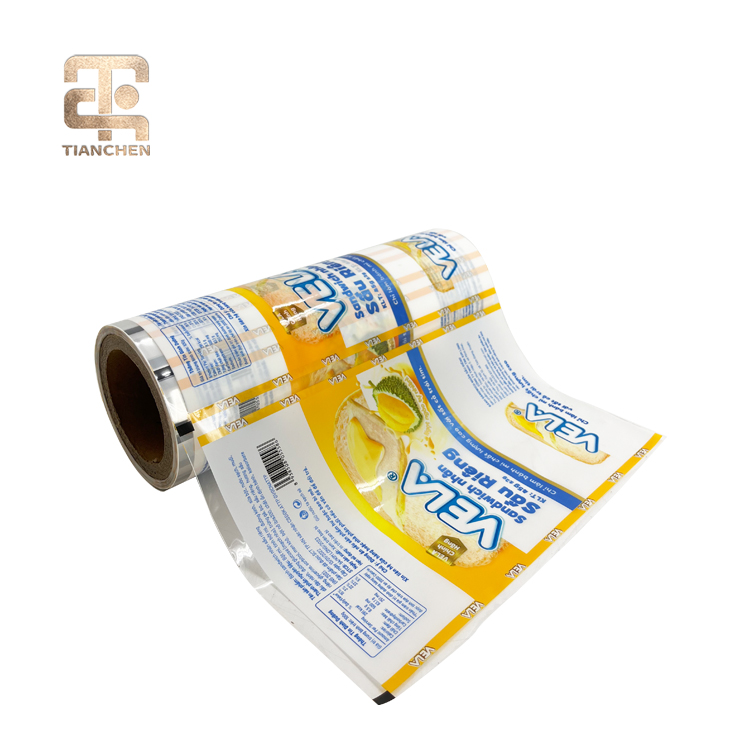
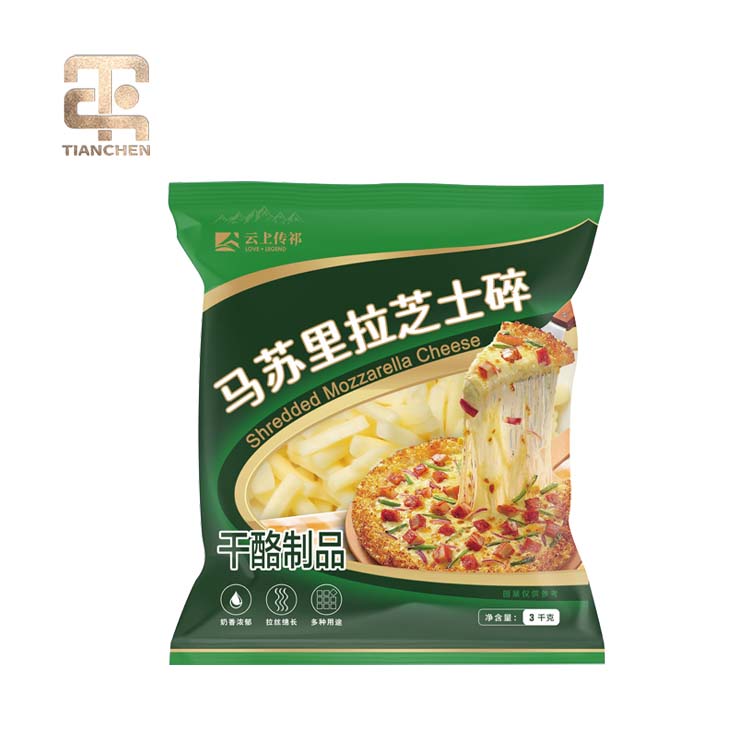
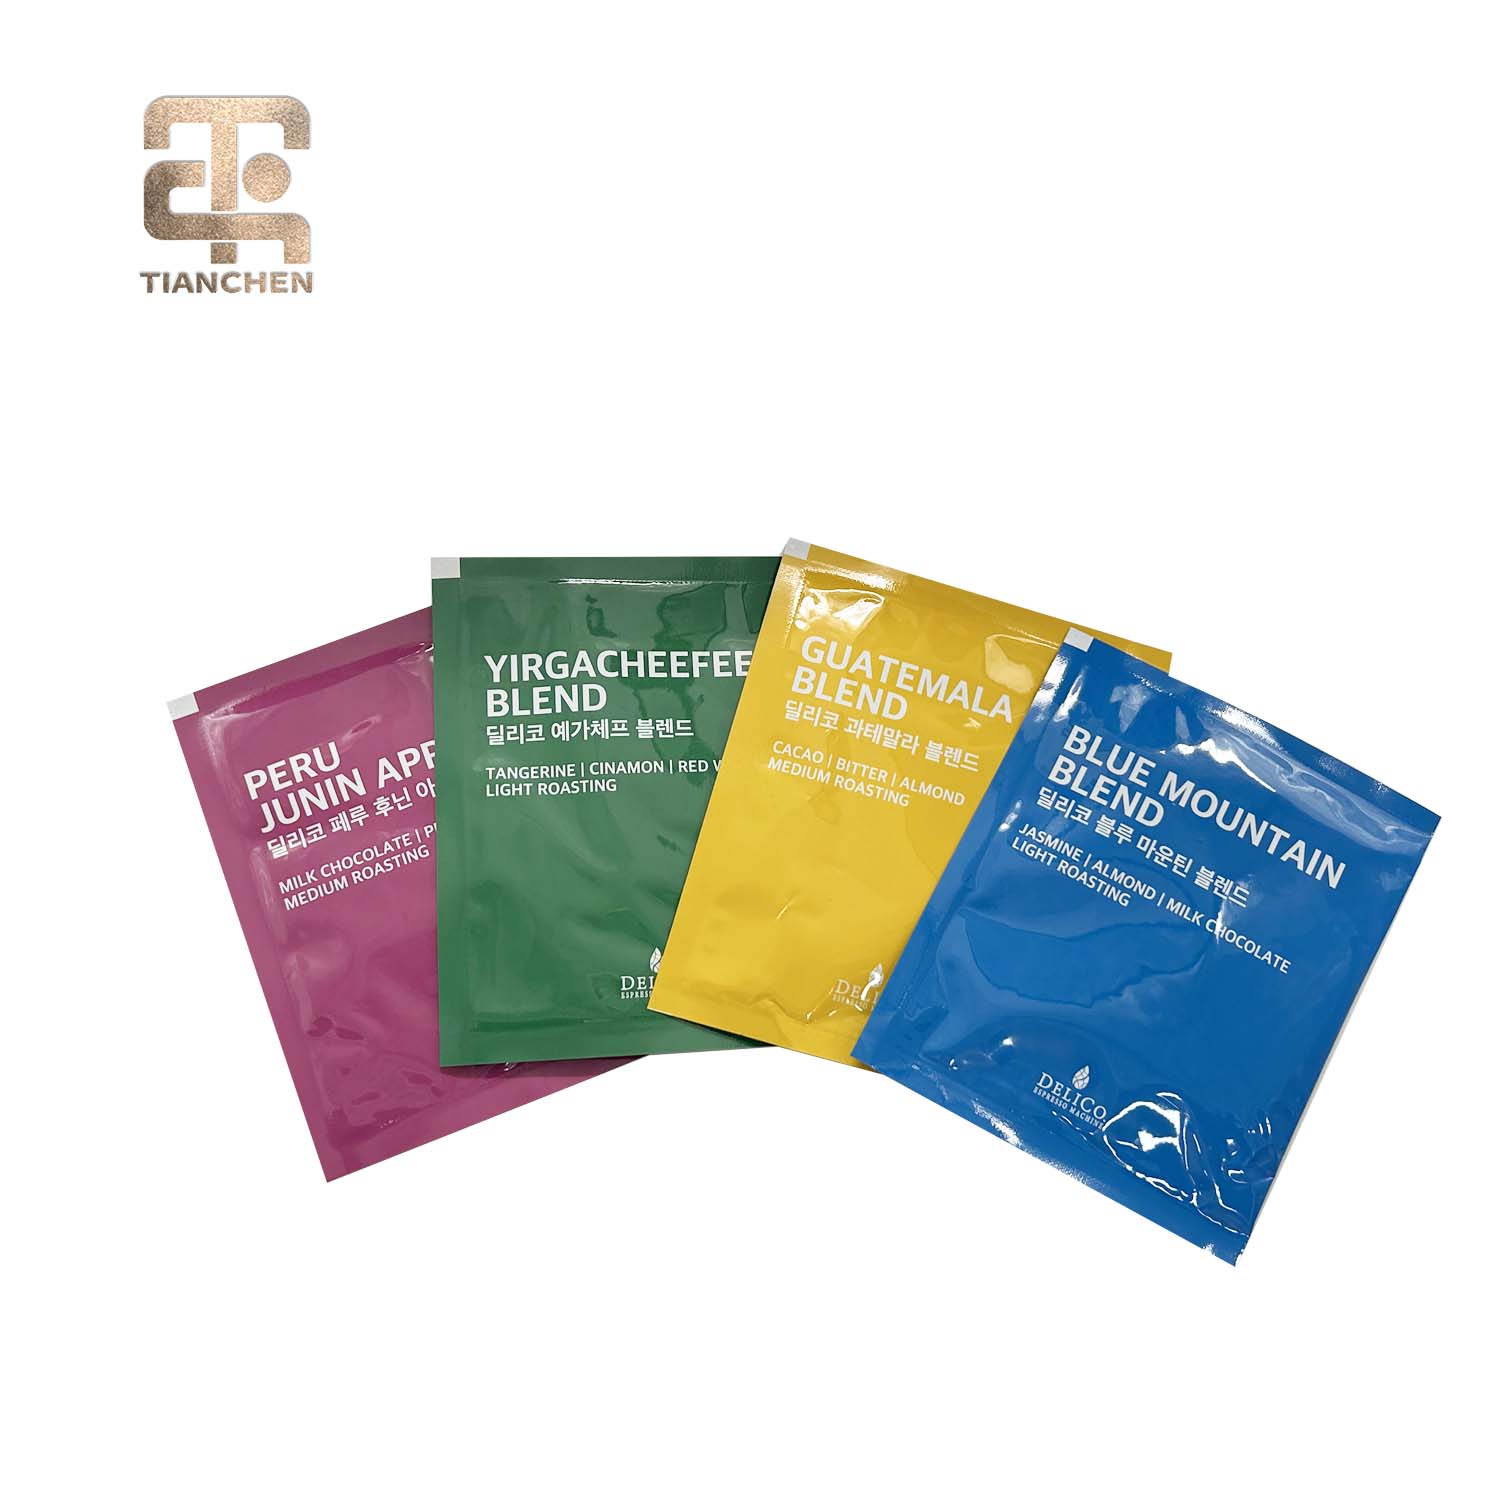
From pillow bags to stand-up pouches, from single-serve sachets to bulk industrial rolls — laminated film delivers tailored performance across every snack food packaging format.
High-speed VFFS pillow bag production for potato chips and extruded snacks demands laminated film with precise COF (coefficient of friction), excellent machinability, and superior oil-resistance. Metallized PET layers provide the light and oxygen barrier needed to maintain crunch for 12+ months.
Premium nut and dried fruit brands require stand-up pouches with resealable zippers, high-clarity windows, and matte surface finishes. Custom laminated structures combining BOPA (nylon) for puncture resistance and LDPE for seal performance are the preferred solution.
Bread, croissants, and baked snacks require packaging that prevents moisture migration in both directions — keeping the product soft while blocking external humidity. Laminated roll films with PE/BOPP or PE/Paper/PE structures are widely used on horizontal flow-wrap machines.
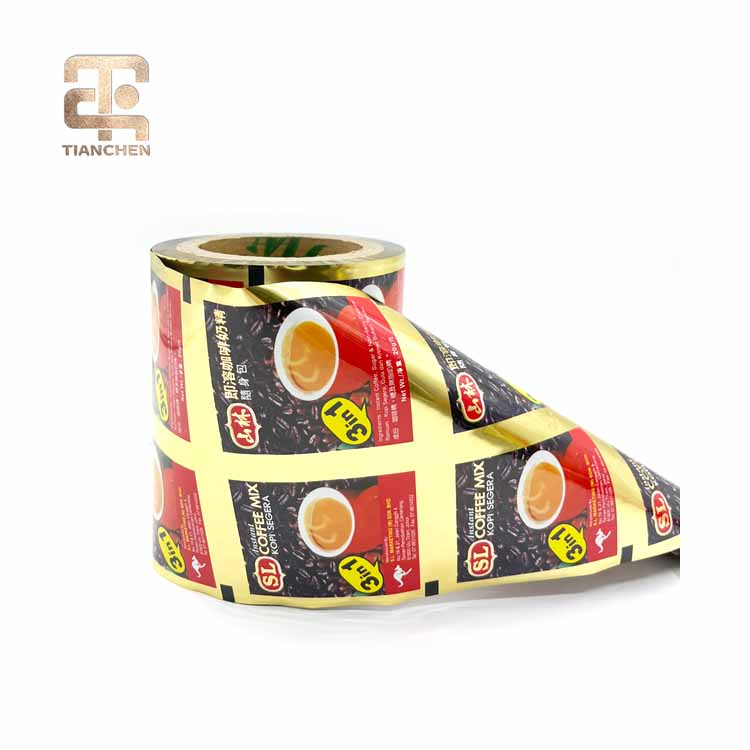
Instant coffee, protein powders, and flavored drink mixes demand the ultimate oxygen and moisture barrier. PET/AL/PE or PET/AL/CPP laminated structures deliver hermetic sealing, aroma retention, and the premium metallic aesthetic that commands retail shelf authority.
Chocolate bars, candies, and gummies require laminated film with exceptional print fidelity for vibrant brand graphics, combined with grease resistance and anti-blocking properties. BOPP/CPP and OPP/PE structures are standard across global confectionery lines.
Frozen snack products — from dumplings to ice cream bars — require laminated films that maintain flexibility, seal integrity, and print quality at temperatures as low as -40°C. Specialized BOPA/PE or BOPET/LLDPE structures are engineered for these extreme conditions.
The booming organic and natural snack segment demands packaging that aligns with brand values. Compostable PLA-based laminates, recyclable all-PE structures, and paper-based laminates with bio-coatings are enabling snack brands to achieve their sustainability commitments without sacrificing performance.
Large-format snack manufacturers and contract packers require industrial-grade laminated film rolls in widths up to 1,300mm, with precise tension control and consistent winding quality to support 24/7 automated production. Our factory supplies master rolls and slit rolls to exact specifications.
Your trusted partner for premium laminated film solutions — serving snack food manufacturers across 5 continents for over 20 years.
We are a professional printing team boasting more than 20 years of profound experience in the flexible packaging industry. Rooted in Guangdong, a hub of manufacturing and international trade in China, Tianchen Printing has grown into a reliable partner for global clients by focusing on rotogravure printing, laminating, and converting services for flexible packaging solutions.
Our business covers a diverse range of industries worldwide, including food and beverage, pharmaceuticals, daily chemicals, electronics, and agriculture. We tailor packaging solutions to meet the unique needs of each sector, from moisture-proof packaging for snacks to high-barrier films for pharmaceuticals, ensuring product safety, shelf appeal, and transportation stability. Over the years, we have established long-term cooperative relationships with clients from Europe, North America, Southeast Asia, and other regions, winning wide recognition for our consistent quality and professional service.
Industries Served: Food & Beverage · Pharmaceuticals · Daily Chemicals · Electronics · Agriculture
Core Capabilities: Rotogravure Printing · Dry Laminating · Extrusion Laminating · Slitting & Converting · Custom Design
Certifications: ISO 9001 · BRC · FDA Compliant · SGS Tested
Innovation · Internationalization · Integration · Intelligentization
Guided by our core four "IN" concepts, we have forged a clear development path and maintained steady growth in the competitive global market. We persist in investing in R&D, upgrading printing technologies and processes, and developing eco-friendly, high-performance packaging materials to keep pace with industry trends and client demands.
We adhere to global standards in production and management, obtain international certifications, and expand our global service network to integrate into the international mainstream market — making us a truly world-class flexible packaging partner for snack food manufacturers worldwide.
Our one-stop service model integrating design, printing, laminating, converting, and quality inspection streamlines the production process, reduces costs for clients, and ensures efficient delivery. By optimizing the industrial chain layout, we bring unmatched efficiency to your snack food packaging supply chain.
We have introduced advanced intelligent production equipment and digital management systems, realizing automated operations in key links such as color matching and quality control, which improves production efficiency and product consistency — delivering the precision your snack food packaging demands.
Advanced rotogravure printing and laminating equipment, operated by experienced technicians, ensures every roll of snack food laminated film meets the highest international standards.


With dedicated R&D investment, ISO-certified production processes, and a team of packaging engineers who understand the unique demands of snack food manufacturing — from high-speed form-fill-seal compatibility to food-contact safety compliance — Tianchen Printing delivers laminated film solutions that help your brand perform better on shelf, on the production line, and in the hands of consumers. Our flexible minimum order quantities, rapid sampling turnaround, and global logistics network make us the ideal long-term partner for snack food brands of all sizes.
Contact our packaging specialists today for custom laminated film samples, technical specifications, and competitive pricing tailored to your snack food production requirements.
Request a Free Sample & QuoteExplore our full portfolio of custom laminated roll films and snack packing films — engineered for every snack food packaging format and production environment.