
Leave Your Message
Explore our precision-engineered aluminum foil films and sachets — purpose-built for beverage, juice, and liquid food brands demanding superior barrier performance.
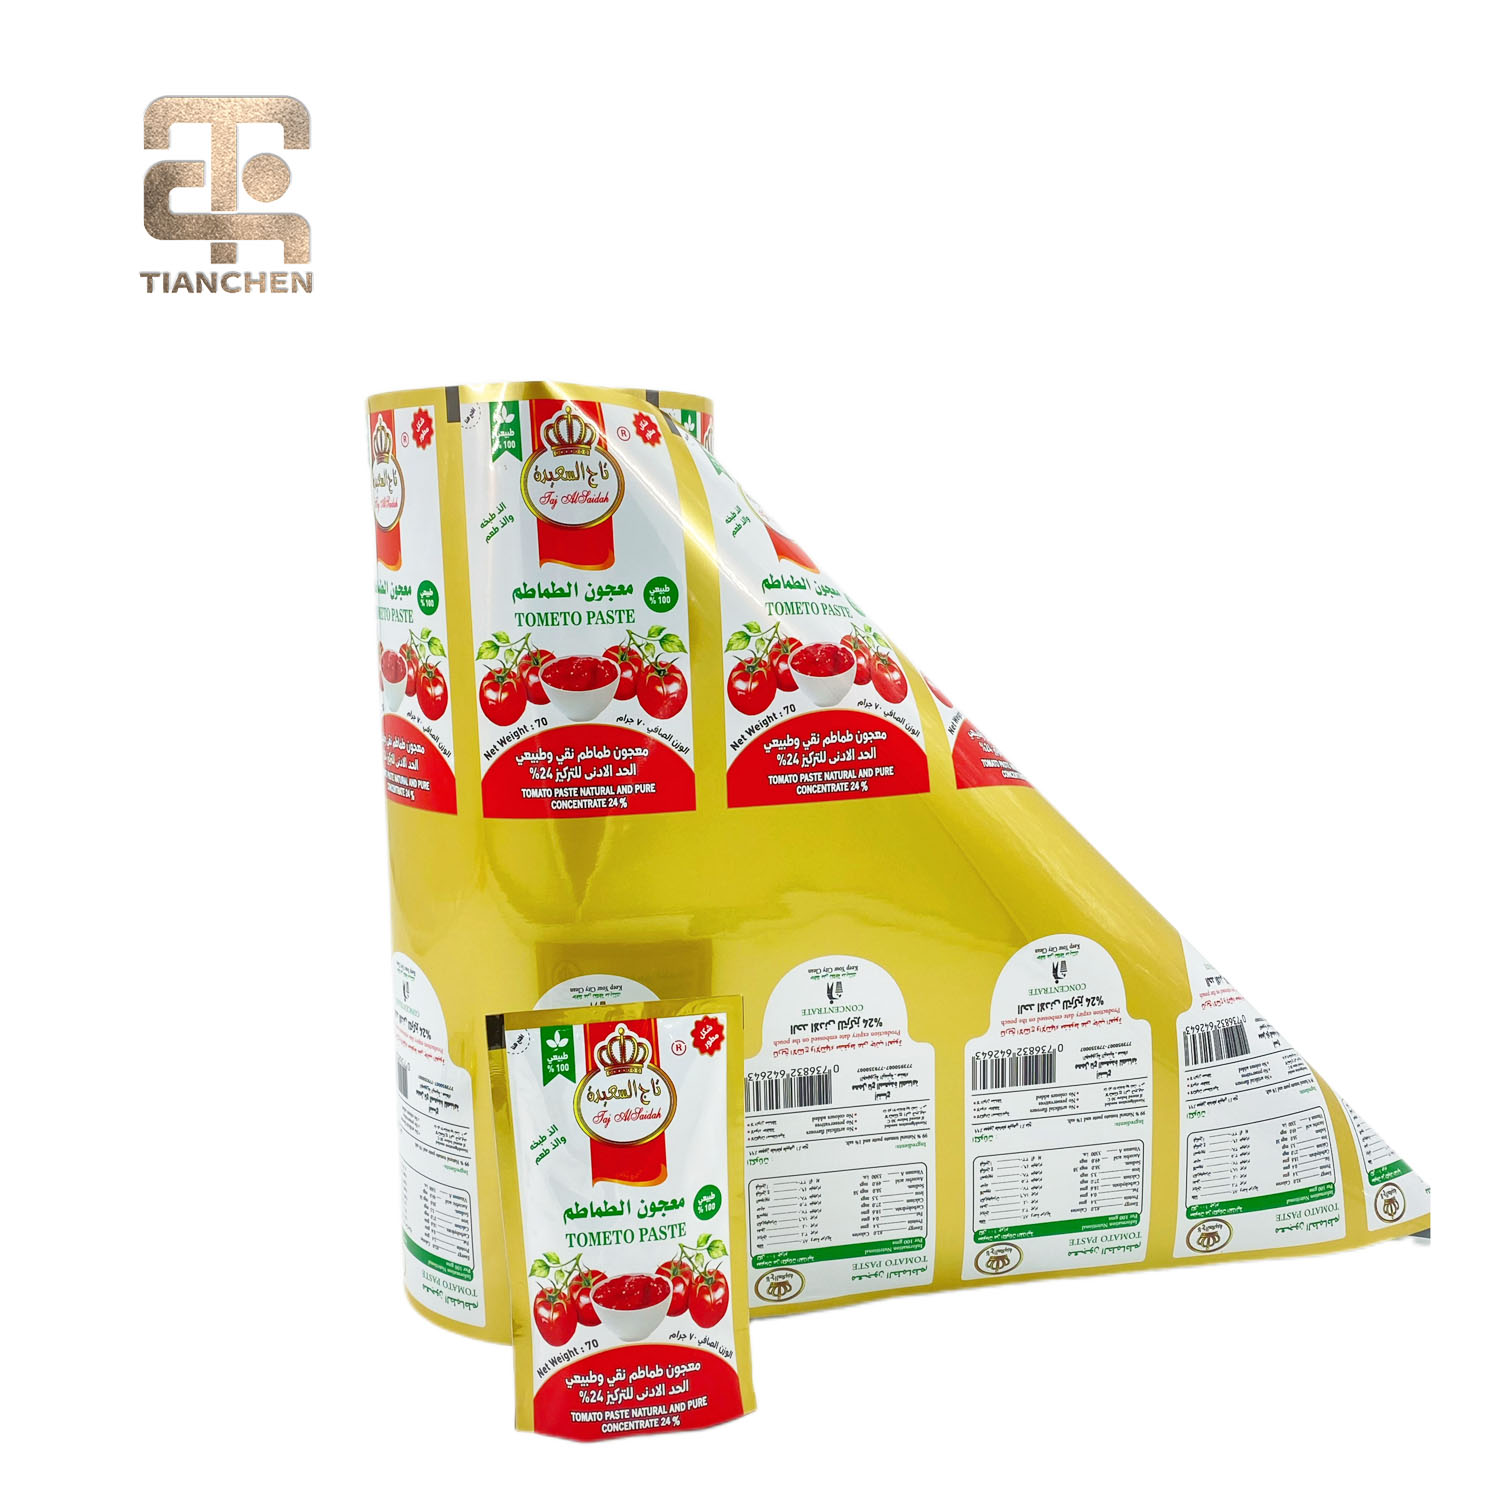
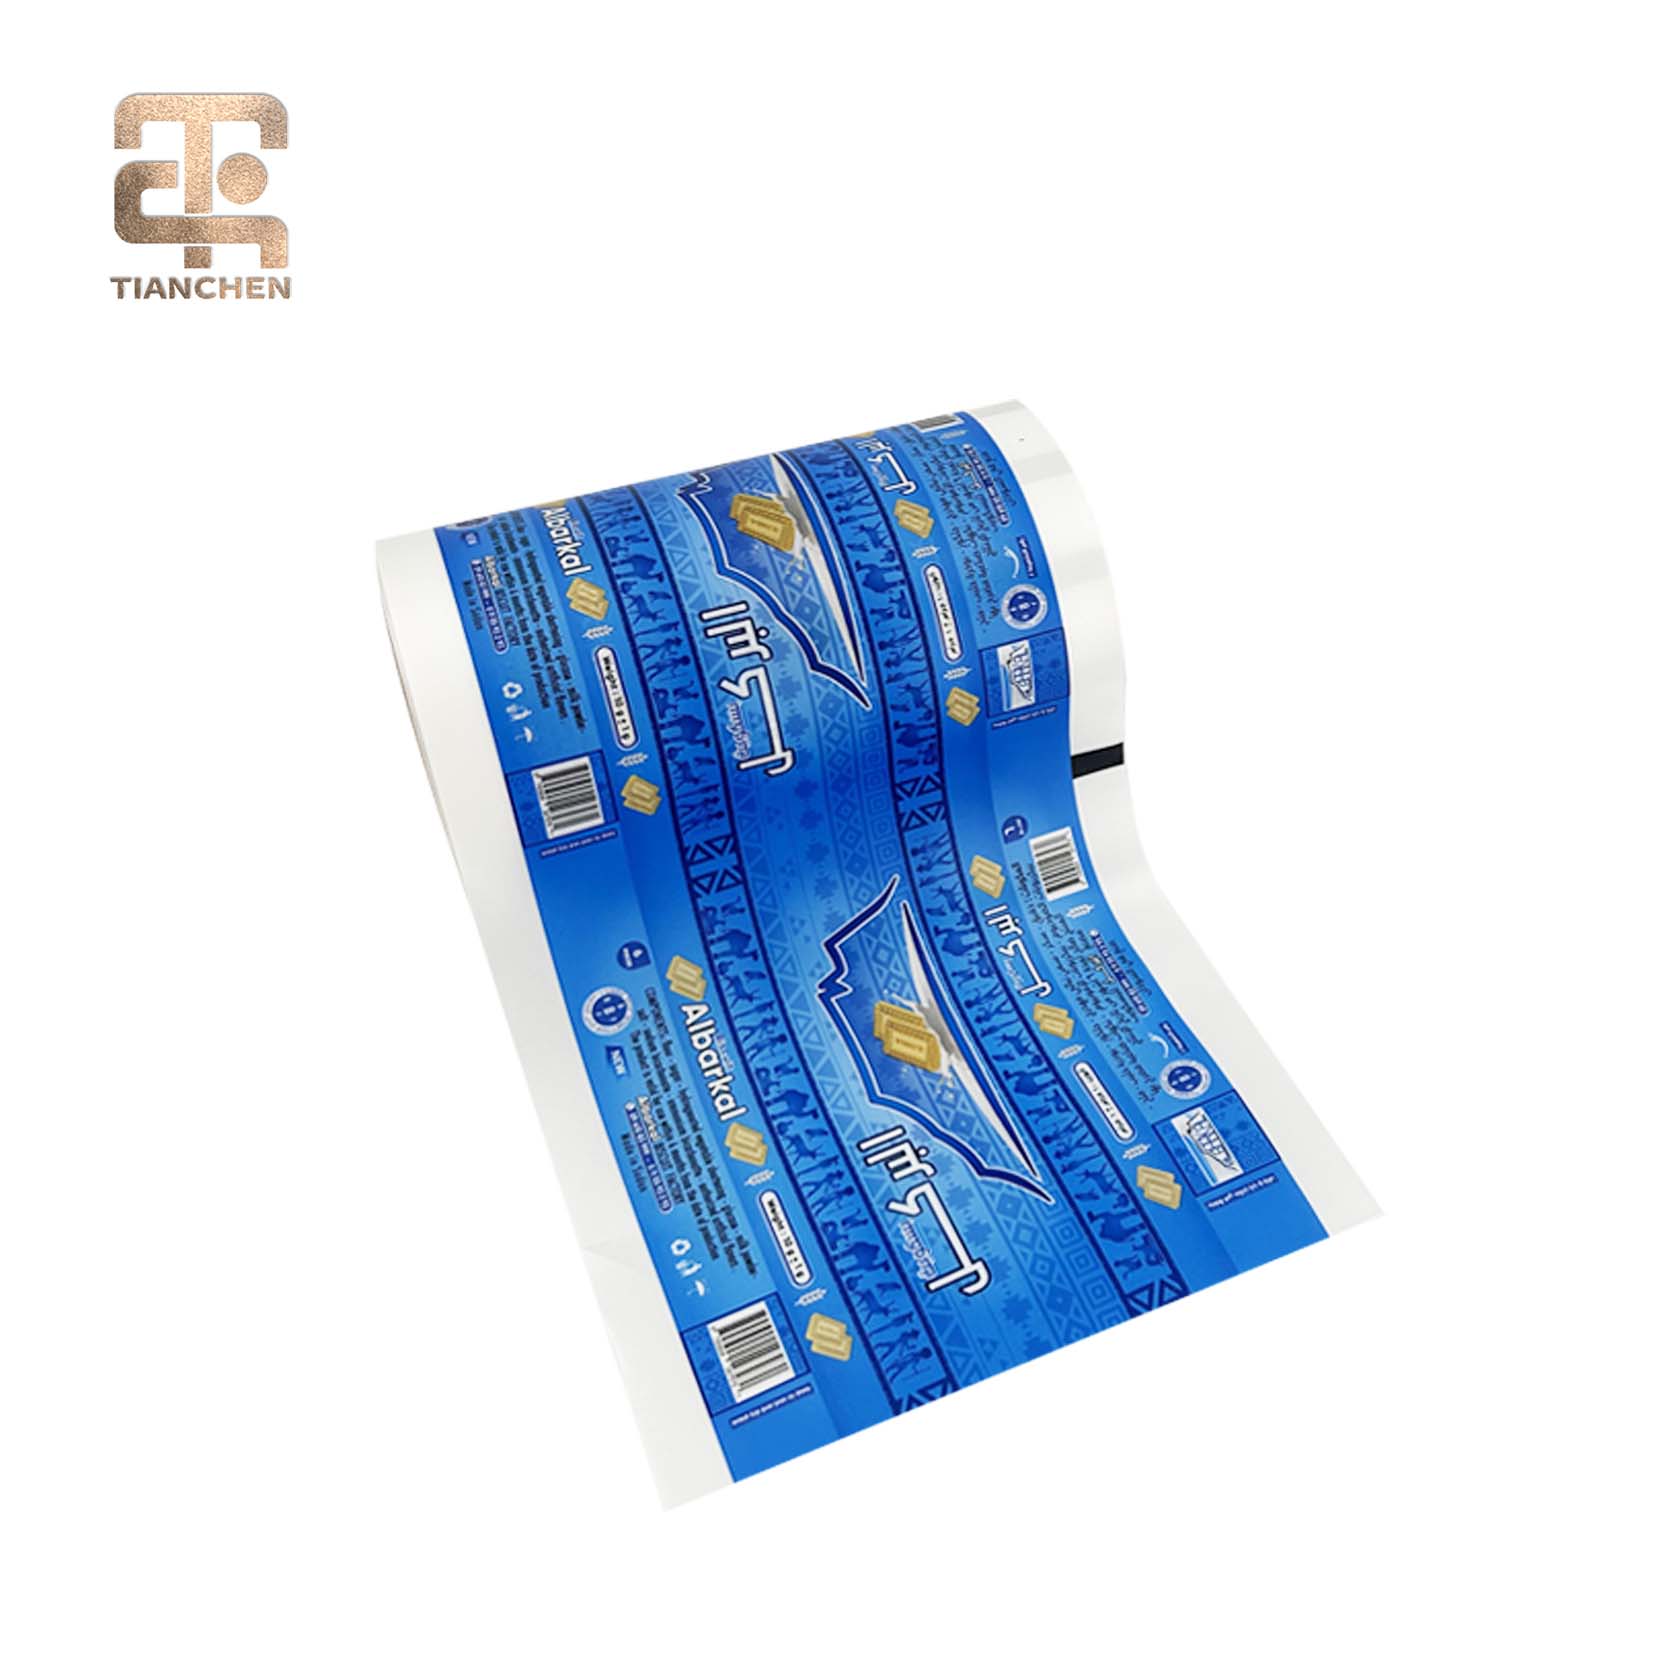

In the modern beverage and juice industry, packaging is far more than a container — it is a critical technological interface between the product and the consumer. Sealing aluminum foil has become the undisputed material of choice for leading beverage and juice brands worldwide, owing to its unmatched combination of barrier properties, printability, formability, and food safety compliance. Whether it is a ready-to-drink juice pouch, a single-serve flavored water sachet, an energy drink multi-layer laminate, or a premium cold-pressed juice stand-up pack, aluminum foil sealing film is the invisible guardian that preserves flavor, nutrients, and brand integrity from the production line to the consumer's hands.
The global flexible packaging market for beverages is projected to surpass USD 38 billion by 2030, with aluminum foil-based laminates accounting for a significant and growing share. This growth is driven by the rapid expansion of the ready-to-drink (RTD) segment, the premiumization of juice brands, and the increasing consumer demand for convenient, portable, and sustainable packaging formats. Brands that invest in high-quality aluminum foil sealing solutions gain a measurable competitive advantage in shelf life, visual appeal, and consumer trust.
At the industrial level, sealing aluminum foil for beverages is not a single material but a sophisticated laminate system. Typical constructions for juice and beverage applications include PET / Al / PE, BOPP / Al / LLDPE, and PET / Al / CPP structures, each engineered to deliver specific performance profiles — from ultra-high oxygen barrier for sensitive cold-pressed juices to high-gloss surfaces for premium brand printing. The aluminum layer, typically between 7 and 12 microns, provides the core barrier function, while the outer layers deliver printability, mechanical strength, and heat-sealability.
The beverage and juice sector is one of the most demanding segments for flexible packaging. Products range from high-acid citrus juices that aggressively attack packaging materials to oxygen-sensitive green teas and cold-brew coffees that require near-zero oxygen transmission rates (OTR). The commercial pressure on packaging suppliers is intense: brands require consistent quality across millions of units, rapid SKU changeovers to accommodate seasonal flavors, and packaging that performs flawlessly on high-speed filling lines running at 200–600 packs per minute.
Aluminum foil sealing films must meet an increasingly stringent set of commercial requirements. Food safety certifications such as FDA, EU Regulation 10/2011, and GB standards are baseline requirements. Beyond compliance, brands demand precise color registration for gravure-printed graphics, consistent seal strength across temperature and humidity variations, and compatibility with a wide range of filling technologies including aseptic, hot-fill, and cold-fill processes. The ability to supply consistent, certified, high-performance aluminum foil sealing film at scale is what separates leading packaging manufacturers from commodity suppliers.
Every layer of our aluminum foil sealing film is engineered to deliver measurable performance benefits for beverage and juice brand owners.
Aluminum foil laminate achieves OTR values below 0.01 cc/m²/day and WVTR below 0.01 g/m²/day, effectively eliminating oxidation and moisture ingress that degrade juice flavor, color, and vitamin content over time.
Up to 10-color rotogravure printing delivers photographic-quality brand graphics, vibrant colors, and precise registration — essential for premium juice and beverage brands competing for shelf impact in global retail environments.
Engineered heat-seal layers ensure consistent, strong seals across a wide temperature range, preventing leakage and contamination in both hot-fill and aseptic filling processes — critical for juice and beverage safety compliance.
We offer recyclable mono-material laminate structures and reduced-gauge aluminum foil options that maintain barrier performance while reducing material consumption — aligning with global brand sustainability commitments and ESG targets.
All aluminum foil sealing films are produced under strict food safety management systems, with compliance to FDA, EU 10/2011, and China GB standards — enabling beverage brands to enter regulated markets with confidence.
Precision dimensional tolerances, consistent COF values, and optimized surface treatments ensure smooth, jam-free performance on high-speed VFFS, HFFS, and pouch-filling machines used in large-scale beverage production.
From fresh-pressed juices to functional energy drinks, aluminum foil sealing technology serves diverse and demanding beverage applications.
The application of sealing aluminum foil in the beverage and juice industry spans a remarkably diverse range of product categories and packaging formats. Understanding these specific application scenarios is essential for brand owners and packaging engineers selecting the right material structure and specification for their products.
Single-serve juice pouches and sachets represent one of the fastest-growing segments in the global beverage market, particularly in Asia, Africa, and Latin America. These formats demand aluminum foil sealing films with exceptional puncture resistance, high seal strength, and outstanding graphics capability. A typical structure for RTD juice sachets is PET12 / Al9 / PE80, providing a robust barrier against oxygen and light while enabling high-speed form-fill-seal production. The aluminum foil layer prevents the photo-oxidation that degrades vitamin C and natural pigments in fruit juices, extending shelf life to 6–18 months at ambient temperature without refrigeration.
Cold-brew coffee and premium tea beverages are among the most oxygen-sensitive products in the beverage category. Even trace levels of oxygen (above 0.1 ppm) can cause flavor staling, color degradation, and loss of antioxidant compounds within days. Aluminum foil sealing films for this category are typically specified with the thinnest possible foil gauge (7–9 microns) to maximize flexibility while maintaining the critical oxygen barrier. Multi-layer structures incorporating PET / Al / CPP or BOPP / Al / LLDPE are standard, with additional matte or soft-touch surface finishes that communicate the premium positioning of artisan cold-brew and specialty tea brands on retail shelves.
The energy drink and functional beverage segment demands packaging that protects active ingredients — vitamins, amino acids, adaptogens, and botanical extracts — from degradation while projecting a bold, high-energy visual identity. Aluminum foil sealing films with metallic or holographic print finishes are widely used in this segment to create visually striking shelf presence. From a technical standpoint, the packaging must withstand the aggressive chemical environment of high-acid, carbonated, or vitamin-fortified formulations without delamination or migration of packaging materials into the product.
Aseptic packaging for long-life juices, dairy beverages, and plant-based drinks relies critically on aluminum foil as the primary barrier layer. In aseptic filling processes, the packaging material is sterilized separately from the product, then filled in a sterile environment. The aluminum foil layer must maintain its integrity through the sterilization process and provide an absolute barrier against microbial ingress throughout the product's shelf life of 6–24 months. Aluminum foil thickness in aseptic beverage applications is typically 6–9 microns, laminated into complex multi-layer structures with paperboard and polyethylene.
The premium organic and cold-pressed juice segment demands packaging that communicates natural, clean-label values while delivering the highest possible barrier performance. Stand-up pouches with spouts, using aluminum foil laminate structures, have become the preferred format for this category. The packaging must be BPA-free, compliant with organic product certification requirements, and capable of showcasing high-quality brand printing. Increasingly, brands in this segment are specifying recyclable or compostable aluminum foil alternatives that maintain barrier performance while meeting sustainability commitments.
The beverage packaging landscape is evolving rapidly. These are the defining trends driving innovation in aluminum foil sealing technology.
Global regulatory pressure and consumer demand are accelerating the shift toward recyclable and reduced-material aluminum foil laminates. Leading packaging manufacturers are developing mono-material structures and ultra-thin foil constructions that maintain barrier performance while reducing the environmental footprint of beverage packaging. The EU Packaging and Packaging Waste Regulation (PPWR) and similar legislation worldwide are setting mandatory recyclability targets that will fundamentally reshape aluminum foil laminate design by 2030.
While rotogravure printing remains the gold standard for large-run beverage packaging, the integration of digital printing capabilities is enabling brands to achieve shorter runs, faster time-to-market, and personalized packaging at commercially viable costs. Hybrid printing systems that combine gravure quality with digital flexibility are increasingly being adopted by forward-thinking packaging converters serving innovative beverage brands that launch multiple seasonal or limited-edition SKUs per year.
The integration of smart packaging technologies — including QR codes, NFC chips, and time-temperature indicators — with aluminum foil sealing films is opening new dimensions of consumer engagement and supply chain transparency for beverage brands. Simultaneously, active barrier technologies incorporating oxygen scavengers and moisture absorbers within the laminate structure are being adopted for ultra-premium juice and functional beverage products, extending shelf life beyond what passive aluminum foil barriers alone can achieve.
The industrialization of AI-driven vision inspection systems, automated defect detection, and real-time color management in aluminum foil printing and laminating is raising the quality bar across the entire beverage packaging supply chain. Leading manufacturers are investing in Industry 4.0 production platforms that enable end-to-end digital quality traceability, from raw material receipt through to finished roll dispatch — providing beverage brands with unprecedented supply chain confidence and regulatory documentation capability.
Beverage brands across all price tiers are investing in premium packaging aesthetics — matte finishes, soft-touch coatings, metallized effects, and spot UV — to differentiate products in an increasingly crowded market. Aluminum foil sealing films are uniquely positioned to deliver these premium visual and tactile effects, and packaging converters that can reliably execute complex multi-finish gravure printing on aluminum foil laminates command significant commercial premiums in the beverage packaging market.
Rapid urbanization and rising disposable incomes in Southeast Asia, Sub-Saharan Africa, and Latin America are driving explosive growth in packaged beverage consumption. These markets have distinct packaging requirements — smaller serve sizes, tropical climate performance, cost-sensitivity — that are driving the development of localized aluminum foil sealing film specifications. Chinese packaging manufacturers with global supply chains and technical expertise are increasingly well-positioned to serve these high-growth emerging markets at competitive price points.
For beverage and juice brand owners sourcing aluminum foil sealing films, the selection of the right manufacturing partner is a strategic decision with long-term implications for product quality, supply reliability, and brand equity. Key evaluation criteria include: demonstrated experience in beverage-specific laminate structures, food safety certification portfolio (FDA, EU, BRC, ISO 22000), gravure printing capability and color management systems, technical support for packaging structure optimization, and the ability to scale from trial volumes to full commercial supply without quality deviation.
China-based manufacturers with modern rotogravure printing and laminating facilities, combined with English-language export capabilities and global logistics networks, offer beverage brands a compelling combination of technical capability, quality, and cost competitiveness. When evaluating Chinese packaging suppliers, beverage brands should prioritize manufacturers with verifiable quality management systems, transparent factory audit records, and a proven track record of supplying regulated export markets in Europe and North America.
Your trusted manufacturing partner for aluminum foil sealing films and flexible packaging solutions — serving beverage and juice brands worldwide for over 20 years.
We are a professional printing team boasting more than 20 years of profound experience in the flexible packaging industry. Rooted in Guangdong, a hub of manufacturing and international trade in China, Tianchen Printing has grown into a reliable partner for global clients by focusing on rotogravure printing, laminating, and converting services for flexible packaging solutions.
Our business covers a diverse range of industries worldwide, including food and beverage, pharmaceuticals, daily chemicals, electronics, and agriculture. We tailor packaging solutions to meet the unique needs of each sector, from moisture-proof packaging for snacks to high-barrier films for pharmaceuticals, ensuring product safety, shelf appeal, and transportation stability.
Over the years, we have established long-term cooperative relationships with clients from Europe, North America, Southeast Asia, and other regions, winning wide recognition for our consistent quality and professional service.

Innovation · Internationalization · Integration · Intelligentization
Guided by our core four "IN" concepts, we persist in investing in R&D, upgrading printing technologies and processes, and developing eco-friendly, high-performance packaging materials to keep pace with industry trends and client demands. For beverage and juice brands, this means continuously advancing our aluminum foil laminate structures to deliver better barrier performance, lighter weight, and enhanced sustainability.
We adhere to global standards in production and management, obtain international certifications, and expand our global service network to integrate into the international mainstream market. Our aluminum foil sealing films for beverage applications comply with FDA, EU 10/2011, and relevant Chinese GB food contact material standards, enabling our clients to access regulated markets across North America, Europe, and beyond with full regulatory confidence.
Our one-stop service model integrates design, printing, laminating, converting, and quality inspection. By optimizing the industrial chain layout, we streamline the production process, reduce costs for clients, and ensure efficient delivery. For beverage brands, this means a single trusted partner managing the entire aluminum foil sealing film supply chain — from structural design and color proofing to full-scale production and export logistics.
We have introduced advanced intelligent production equipment and digital management systems, realizing automated operations in key links such as color matching and quality control, which improves production efficiency and product consistency. AI-driven inline inspection systems monitor every meter of aluminum foil sealing film produced, ensuring that beverage brands receive only materials that meet their precise specifications — every roll, every order.
Our Guangdong production base is equipped with advanced rotogravure printing presses, dry-laminating machines, and intelligent quality inspection systems — purpose-built for high-volume beverage packaging production.


Guided by our core four "IN" concepts, we have forged a clear development path and maintained steady growth in the competitive global market. Innovation drives our R&D investment in new aluminum foil laminate structures for beverage applications. Internationalization ensures our products meet the highest global food safety and regulatory standards. Integration delivers end-to-end supply chain efficiency. And Intelligentization guarantees the consistent, defect-free quality that global beverage brands demand.
The third concept is Integration, which refers to our one-stop service model integrating design, printing, laminating, converting, and quality inspection. By optimizing the industrial chain layout, we streamline the production process, reduce costs for clients, and ensure efficient delivery. The fourth is Intelligentization — we have introduced advanced intelligent production equipment and digital management systems, realizing automated operations in key links such as color matching and quality control, which improves production efficiency and product consistency.
From PET aluminum foil sachets for coffee and juice to metallized film rolls for high-speed beverage lines — our full product range covers every sealing application.
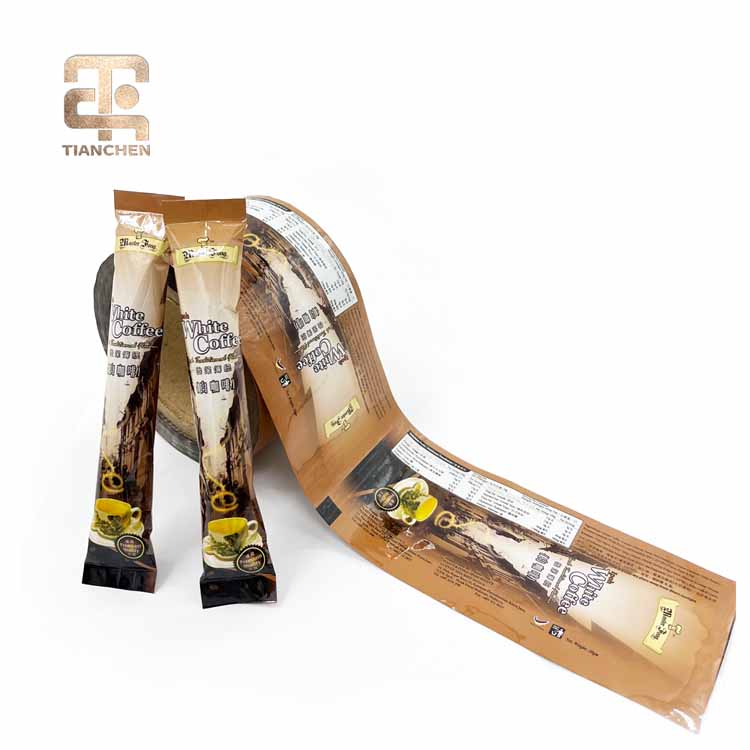
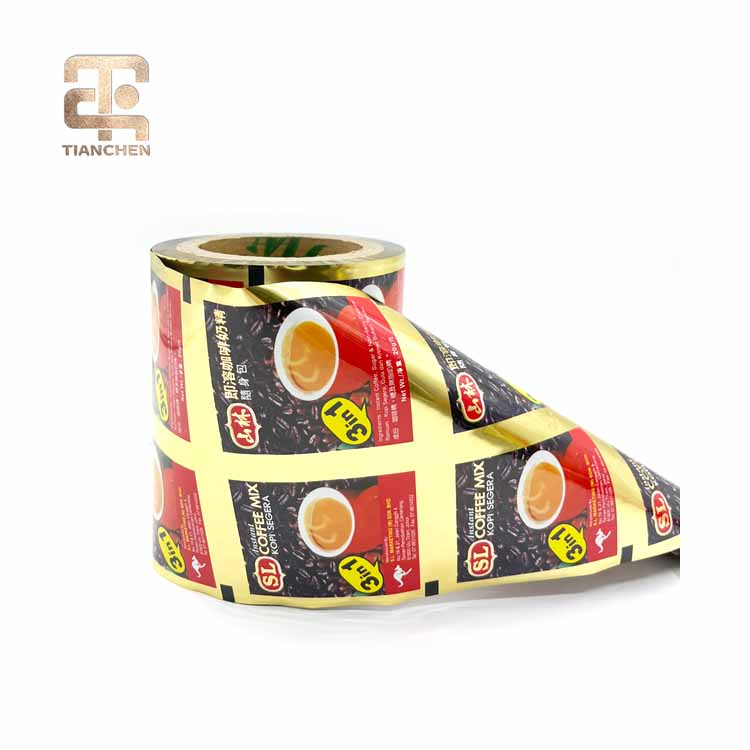
Whether you are launching a new juice brand, scaling an RTD beverage line, or upgrading your aluminum foil sealing film specification, our team is ready to deliver precision-engineered solutions tailored to your exact requirements.
Explore Our Aluminum Foil Sealing Films →